
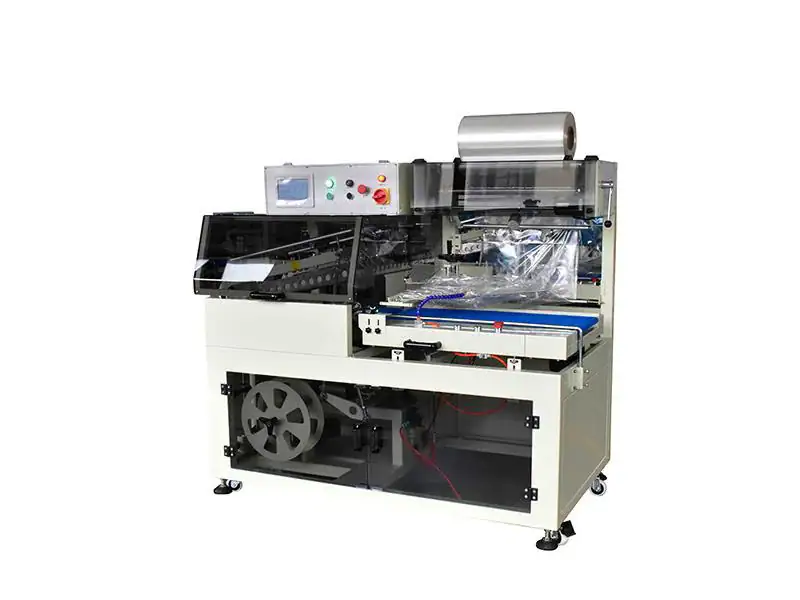

Shrink Wrapping Machine Applications and Maintenance Tips
nnshrink wrapping machines are versatile packaging tools used across numerous industries. Understanding their applications and proper maintenance is key to maximizing your investment.
Common Applicationsshrink wrapping is widely used for product bundling, multi-pack creation, tamper-evident sealing, and protection during transit. Industries benefiting from this technology include food and beverage, pharmaceuticals, cosmetics, and consumer goods.
Maintenance TipsTo keep your shrink packaging machine operating at peak performance:
- Regularly clean the sealing blade to prevent residue buildup
- Check and replace Teflon tape on sealing elements
- Inspect conveyor belts for wear and proper tension
- Monitor shrink tunnel temperature consistency
- Lubricate moving parts according to the maintenance schedule
- Keep the machine clean and free from film scraps
Proper maintenance extends machine life and ensures consistent shrink wrapping quality for years to come.
Shrink Wrapping Applications and Maintenance: 2026 Practical Guide
Shrink wrapping machines are used across food, beverage, pharmaceutical, and consumer goods industries. This guide covers specific application configurations for each industry and a maintenance schedule that extends machine life from 8 to 12+ years.
Industry-Specific Applications
- Food multipacks: Shrink-wrapping 6-12 snack bags together for retail display. Film: 15-micron PVC (clarity for retail visibility). Tunnel temp: 160 degrees Celsius, 8 seconds.
- Beverage can carriers: Replacing plastic rings with shrink film. Film: 50-micron PE (puncture resistance for can tops). Tunnel temp: 180 degrees Celsius, 12 seconds.
- Pharmaceutical cartons: Tamper-evident shrink bands on medicine boxes. Film: 40-micron PETG (complies with EU FMD). Tunnel temp: 140 degrees Celsius, 5 seconds.
- Hardware and tools: Shrink-wrapping tool sets in corrugated trays. Film: 80-micron PE (heavy-duty puncture resistance). Tunnel temp: 200 degrees Celsius, 15 seconds.
Preventive Maintenance Schedule
| Frequency | Task | Time Required |
|---|---|---|
| Daily | Clean film residue from sealing blade | 5 min |
| Weekly | Inspect and clean heat tunnel conveyor belt | 15 min |
| Monthly | Lubricate conveyor bearings and chain | 20 min |
| Quarterly | Replace sealing blade (Teflon-coated) | 30 min |
| Annually | Calibrate temperature sensors, inspect wiring | 2 hours |
Common Issues and Solutions
- Incomplete shrink: Tunnel temperature too low or belt speed too fast. Increase temp by 5 degrees or reduce speed by 10%.
- Film burn-through: Temperature too high for thin film. Reduce temp or switch to thicker film.
- Uneven shrink: Uneven heat distribution. Clean tunnel air outlets and check fan operation.
- Seal failure: Sealing blade worn or dirty. Clean with isopropyl alcohol or replace blade.