
Two Automatic Case Packing Lines for a Brazil Customer: From Flat Blank to Sealed Carton, Tested in Our Workshop Before Crating
In November 2026 we finished building and testing two end-of-line case packing lines for a customer in Brazil. Each line takes a flat corrugated blank, opens it and seals the bottom, moves the empty carton through a packing station, then folds the top flaps and seals the carton with tape. Both lines were run on our floor with the customer’s carton size, the customer watched the test video, confirmed the result in writing, and only then did we move the machines into export wooden cases. This article walks through what was built, how the stations work together, and what the customer actually signed off on.
What the customer ordered and why
The buyer runs two separate packing areas and wanted one line per area rather than a single shared line. The reason is practical: when one area stops for a carton-size change or a routine check, the other keeps running. Two lines also cap the distance operators have to carry filled product. The order was therefore two identical-layout lines, each built around the same four stations: an automatic case erector with bottom sealing, a motorized roller conveyor, a manual loading station where staff place product into the open carton, and an automatic case sealer that folds and tapes the top.
The carton is a standard regular slotted container, and the line is set up for one carton format at a time with a defined changeover between formats. The customer’s stated goal was not peak speed on a single SKU. It was to remove the two slowest manual steps in the room — opening and bottom-taping boxes by hand, and folding and top-taping them after packing — while keeping one person at the loading point to control what goes into each carton.
The line layout, station by station
1. Automatic case erector with bottom sealing
The erector sits at the head of the line. A stack of flat blanks is loaded into the magazine; the machine pulls one blank at a time, squares it around the forming head, and drives the bottom flaps together before the bottom sealing head applies tape. The finished empty carton is discharged square and open at the top, ready to be filled. This station is enclosed in a guarded frame with an HMI and a control panel, which you can see on the right side of the overview video. The enclosure keeps hands away from the pick-off and flap-closing mechanisms while the machine is cycling.
Replacing manual erecting changes the rhythm of the whole room. A person opening boxes by hand is usually the bottleneck the packing station has to wait on. The erector releases a steady stream of open cartons, so the conveyor and the loading staff set the pace instead. It also removes the variation in hand-folded bottoms, which is where poorly squared boxes and tape wrinkles usually start.
The blank magazine is sized to hold a working stack rather than a full shift of board, which keeps the machine footprint down and lets the operator top up blanks during the normal loading cycle. The low-board warning on the HMI alerts the operator before the magazine runs empty, so the line does not finish a cycle and then stop for lack of a blank. Keeping the magazine loaded is a short, frequent task rather than a long interruption, which fits the way the single operator already moves between the conveyor and the loading point.
2. Motorized roller conveyor
Between the erector and the sealer, open cartons travel on a motorized roller conveyor that also forms the manual loading zone. The roller surface is level with the machine infeed and outfeed, so cartons transfer without a lift. Guide rails keep each carton square as it moves. The conveyor is the buffer in the system: it holds a queue of open cartons so the erector can keep cycling while the operator fills the box in front of them, and so a short pause at loading does not stop the erector immediately.
The length of the conveyor is not chosen for the floor plan alone. It sets the size of the buffer between the erector and the loading point. A conveyor that holds three or four open cartons gives the erector enough room to keep cycling when the operator pauses to handle a label or check a pack, and it gives the operator a ready queue so they are never waiting on an empty box. A conveyor that is too short passes every small pause straight back to the erector, which starts and stops repeatedly and loses the steady rhythm it is designed for. On this order the conveyor length was set to hold a small queue while keeping the overall footprint compact for the two packing areas.
3. Manual loading station
The customer deliberately kept this step manual. An automatic case packer with a robotic or drop-in loading head pays back when a single SKU runs at high volume for long stretches. This buyer handles a mix of products and pack counts, and wants a person to verify contents and arrangement before the box is closed. The operator loads product into the open carton as it reaches the station, then releases it toward the sealer. The line is built so this can be upgraded later: the conveyor and sealer are already sized to accept an automatic loading head if the product mix narrows and volume rises.
4. Automatic case sealer, model ZYFC-05
At the end of the line, the filled carton enters the automatic case sealer. The yellow flap-folding arms tuck the four top flaps in sequence, and the top sealing head applies the tape as the carton passes through. The carton exits closed and sealed on both its original bottom tape from the erector and its new top tape. The sealer specified on this order is the ZYFC-05 model, the same unit type whose electrical rating is examined in the technical companion article.
How the flap folding and tape head actually work
A regular slotted carton has four top flaps: two narrow inner flaps and two wider outer flaps. The sealer handles them in a fixed order. As the carton enters, a curved plow lifts the two inner flaps and holds them up; a set of side arms then sweeps the two outer flaps inward and over them, so all four meet in the center. The carton is already moving while this happens, which is why the folding arms are shaped as curves rather than straight bars. By the time the box reaches the tape head, the flaps are held flat and square.
The tape head itself is a simple mechanical unit with no separate motor. A spring-loaded roller presses the leading edge of the tape onto the box, a fixed blade cuts the tape at the correct length as the carton keeps moving, and a rear roller wipes the trailing end down onto the carton. Tape tension is set by an adjustable brake on the roll. If the brake is too tight the tape stretches and pulls away; too loose and the tape lays in wrinkles. This is a setting we fix during the test and mark for the customer, because it is the first thing an operator will check when a box looks poorly sealed.
The carton itself: board grade and why it matters
The machines are built around the carton, not the other way around, so the blank specification is part of the engineering. Corrugated board is described by its flute profile and its strength. The flute is the wavy inner layer: common profiles run from a fine B flute for printed retail boxes through a stiffer C flute for shipping cases, with double-wall BC board used for heavier contents. Strength is stated either as an edge crush test value, which measures the load a standing box can carry before it buckles, or as a Mullen burst value, which measures resistance to puncture. Edge crush figures are the more common choice for warehouse stacking; burst figures matter when contents are sharp or the box is handled roughly.
These details feed directly into the erector settings. A heavier double-wall blank is stiffer, so the magazine suction cups and the forming head need more force and the flap-closing timing is slightly different. A board that is too light for the product weight will crush at the forming head or sag on the conveyor. We ask for the customer’s actual blanks rather than a generic sample so the test runs on the real material, and the test videos in this order were shot with those exact boxes.
How the factory acceptance test was run
Before recording anything for the customer, we ran the line through the same checks we use on every export order. The list below is the practical version, not a paperwork exercise.
- Loaded the erector magazine with a full stack of the customer’s blanks and confirmed it picks one blank at a time without double-feeding or jamming.
- Checked every erected box for square corners and a centered bottom tape, and rejected any box with a folded-in or crushed flap.
- Set the conveyor guide rails and the sealer belt width to the carton dimensions and confirmed the carton does not skew between stations.
- Ran a batch through the sealer and checked that all four top flaps are fully tucked, the tape is centered and bonded, and there are no lifted corners.
- Checked the guarded erector with the doors open and closed to confirm the interlocks stop the cycle when access is opened.
- Measured the electrical draw against the nameplate and confirmed the emergency stop brings the line to a halt from any station.
The customer’s written sign-off
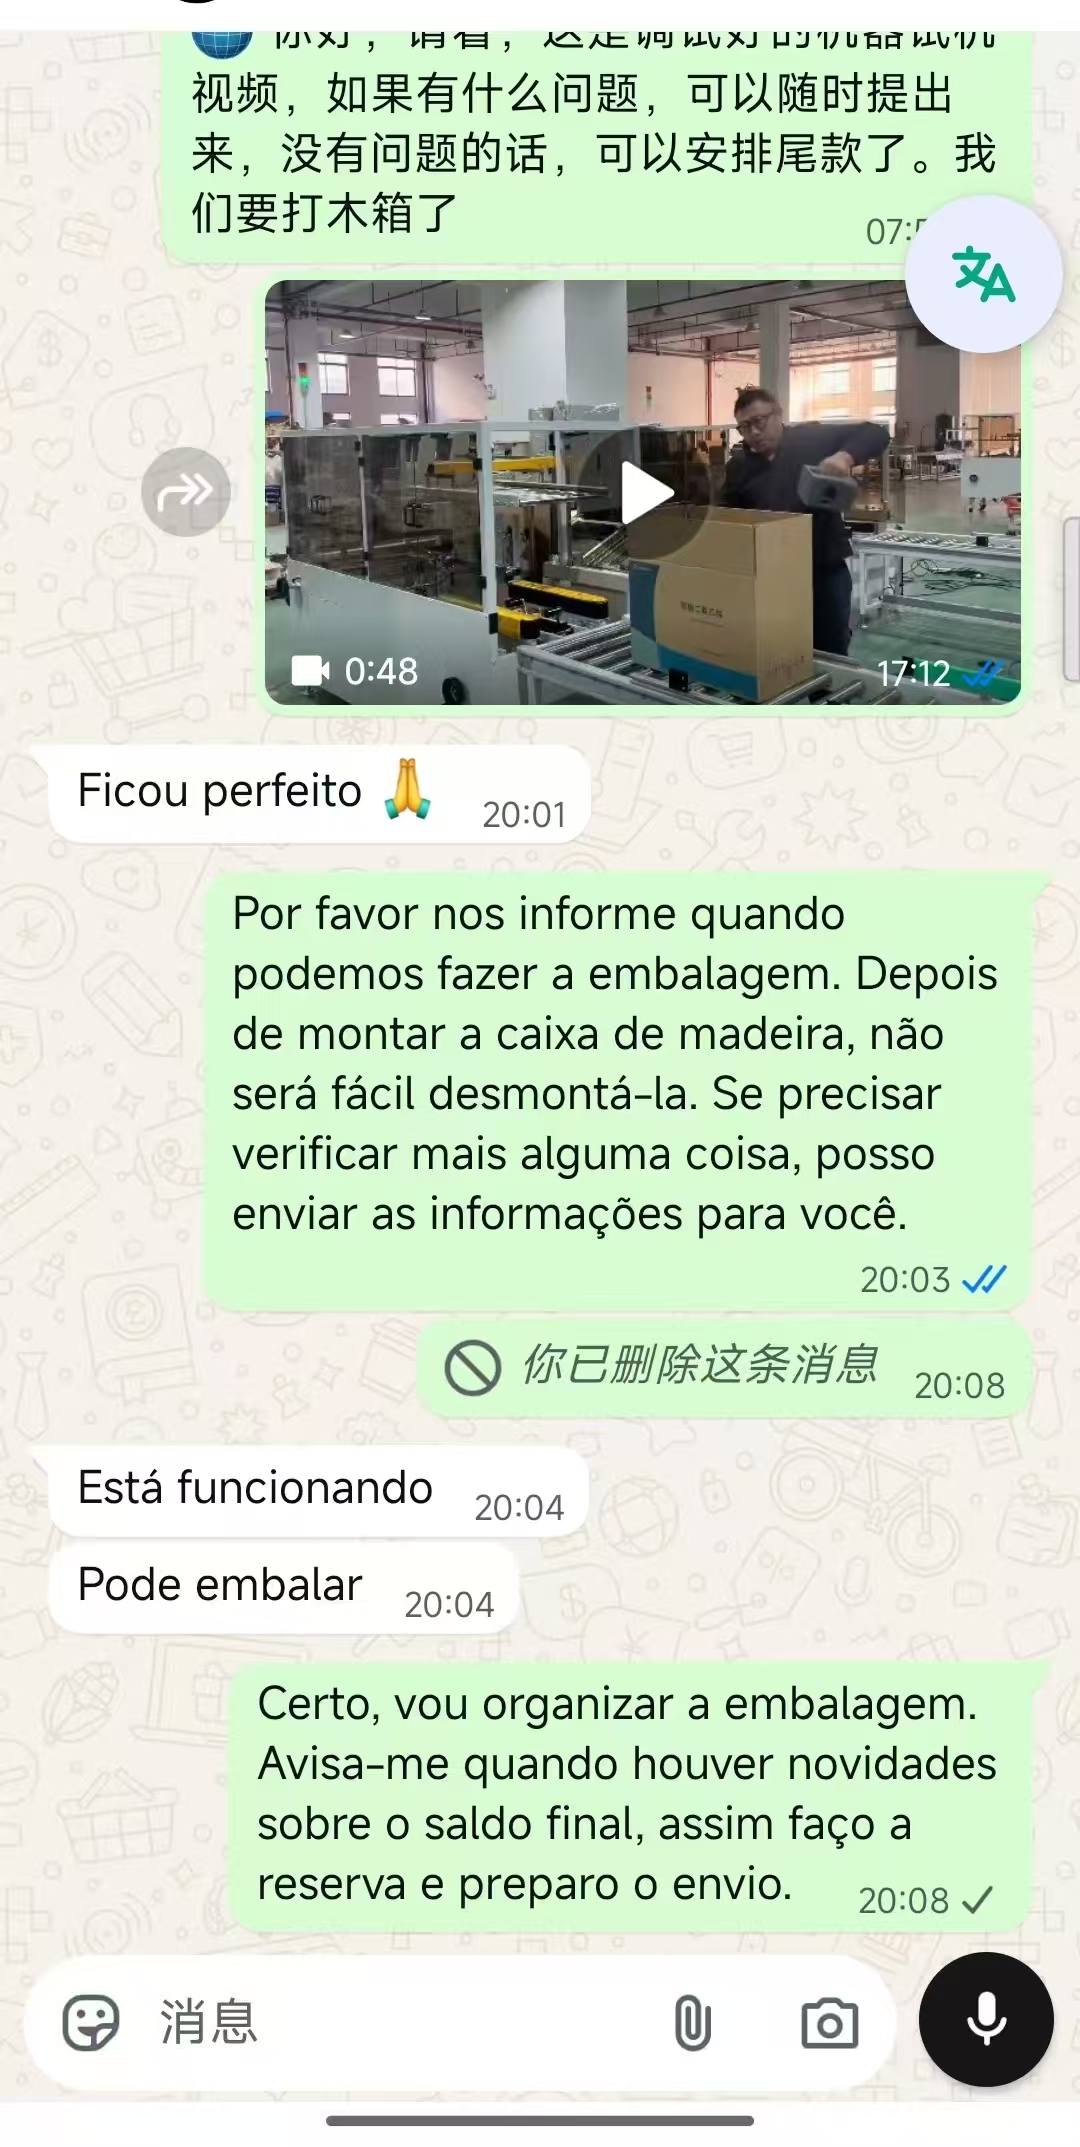
The messages in the screenshot are the customer’s own words. After receiving the test video, the buyer replied “Ficou perfeito” (it came out right), then “Está funcionando” (it is working) and “Pode embalar” (you can pack it). We hold the line on crating until this confirmation is in hand for a simple reason: once a machine is bolted into a wooden export case, opening it back up to check a setting means partly dismantling the packaging. Confirming the test first keeps the customer’s timeline and ours clean.
Automatic line versus the manual process it replaces
| Point of comparison | Manual erect, pack and seal | These two automatic lines |
|---|---|---|
| Erecting and bottom tape | Done by hand, speed varies with the operator | Automatic from the blank magazine, consistent square boxes |
| Top flap folding and tape | Hand folded, tape often off-center or wrinkled | Mechanical folding and centered tape on every box |
| Staff needed per line | Three to four people across the steps | One person at the loading station |
| Box quality variation | High, depends on fatigue and shift | Low, settings fixed until a format change |
| Pace control | Set by the fastest manual step | Set by the loading operator, with a buffer queue |
| Main limitation | Labor cost and inconsistent boxes | One carton format at a time; a changeover is needed between sizes |
How throughput is calculated on a line with a manual station
On this layout the erector and the sealer are both capable of running faster than the manual loading point, so the loading operator sets the real output, not the machine nameplates. The useful calculation is cycle time at the loading station. If the operator can release a filled carton every six seconds, the line is capped at ten cartons per minute regardless of how quickly the erector can cycle. Sizing the machine above that pace is not wasted, but it does not raise output; it builds the buffer queue and lets the erector catch up after a short pause.
The practical way to plan the line is to work backwards from the shift target. Take the number of sealed cartons the shift needs, divide by the working minutes, and then add a margin because no manual station runs at its peak for a full shift. A common planning figure is to size the line against roughly 70 to 80 percent of the operator’s best pace, which leaves room for breaks, minor checks and the occasional misfed box. Building to the theoretical maximum leaves no buffer and the line will miss its target as soon as anything interrupts loading.
Safety guarding and the CE machinery requirements
The hazards on this line are concentrated in two places: the erector’s pick-off and flap-closing mechanisms, which move with real force, and the sealer’s tape blade and drive belts. The erector is therefore built as a guarded cabinet with interlocked doors, so opening access while the machine is cycling stops the motion before a hand can reach the mechanism. The sealer keeps its moving parts behind fixed guards with the tape head reachable only through a defined opening for roll changes. Emergency stop buttons are placed at the erector panel, the loading zone and the sealer, and any one of them stops the complete line.
The CE mark on the nameplate is backed by the declaration in the document pack. The machine is assessed against the machinery directive for mechanical and electrical safety, with the guarding distances, interlock behavior and emergency stop circuit documented rather than assumed. Conveyor pinch points are guarded where a roller meets the drive, and the electrical panel is built to the relevant low-voltage and panel standards. This matters beyond the European market because the customer’s own safety review will ask for the same evidence regardless of destination.
Site preparation and installation
The line does not need a special foundation, but the floor has to be flat and level enough that the frames sit square; the machines use adjustable feet rather than castors in their fixed position. The main site inputs are the electrical supply matching the nameplate and a clear layout that leaves room for the erector magazine to be loaded from the front and for the operator to work the loading station without crossing the conveyor. We provide a dimensioned layout before shipment showing the exact footprint, the access clearance, and where the power is brought in, so the customer can prepare the floor and the supply point before the cases arrive.
On-site commissioning follows a fixed sequence: level and join the sections, connect the conveyor and the inter-station signals, confirm the direction of every drive, run empty cartons through the full path, then run filled cartons and check the seals. The same acceptance points used in the factory test are repeated on site, because transport can shift a guide rail or loosen a setting even when the crating is sound.
Maintenance and the parts that wear
The line uses few wearing parts, which is part of the reason it suits a buyer without a large maintenance team. The consumable is the tape itself, replaced by the operator as a routine. The tape blade dulls over a long period and is a bolt-in replacement rather than a sharpening job. The conveyor drive chains and the sealer drive belts are checked and lubricated on a schedule, and the suction cups on the erector magazine are inspected because a worn cup is the usual cause of a missed pick. The table below covers the faults that actually come up in service.
The order shipped with a defined consumables and spares set rather than an open-ended list. Alongside the machines went the first rolls of the specified BOPP tape, one replacement tape blade per sealer, a spare set of the erector magazine suction cups, and the fixings needed to join the conveyor sections. Keeping these first-service items in the same case as the parts list means the maintenance team does not have to source a holder-specific blade or a matched cup before the first routine service. The parts list itself is keyed to each machine’s serial number, so any later order can be placed against the exact fitted component rather than a description.
| Symptom | Likely cause | Action |
|---|---|---|
| Erector misses a blank or double-feeds | Worn suction cup, or magazine not stacked square | Inspect the cup, re-square the stack and check the air setting |
| Box skews on the conveyor | Guide rail loose or set too wide | Re-set the rails to the carton width and lock them |
| Tape wrinkled or off-center | Tape brake tension wrong, or roller dirty | Re-adjust the brake and clean the pressure roller |
| Top flap not fully tucked | Folding arm height out after a size change | Re-set the arm height to the new carton height |
| Sealer stops with a box jammed inside | Crushed carton or a foreign object in the head | Clear from the access opening, never with the power connected |
Crating and shipment
After the written sign-off, each line was broken down into its transport sections, fixed into fumigated export wooden cases, and braced so the conveyor frames and guarded cabinets cannot move in transit. The control panels and the HMI units are wrapped separately and packed against the frames. The accompanying documentation pack includes the electrical drawings, the parts list keyed to each machine’s serial number, the CE declaration, and the operation and maintenance notes. Because the customer ordered two lines, the cases are marked to show which section belongs to which line so reassembly on site is straightforward.
Receiving the cases and the uncrating checklist
Because the cases are marked line by line, the receiving team can stage each set of crates close to the packing area it belongs to rather than unstacking everything in one bay. The first check on arrival is the external one: confirm the fumigation marks and the case labels are intact, and note any case with a broken brace or a punctured panel before it is opened. If a crate has taken a hard impact in transit, the right move is to open it against the packing list and check the section against the dimensioned layout before power is connected, rather than assume the machine inside is square.
Uncrating follows the document pack in reverse. Each section is checked against the parts list keyed to its serial number, the separately wrapped HMI and control panels are matched to their cabinets, and the bagged fixings and the spare tape blades are counted before the wooden case is broken down. Keeping the packaging until every item on the list is ticked is deliberate: a missing guide-rail clamp or a loose cable is far easier to trace while the case and its markings are still there. Once the inventory is complete, the on-site commissioning sequence already described takes over, beginning with levelling the feet and joining the conveyor sections.
Project timeline and keeping the two lines identical
Building two lines in one order is managed against a single specification so the machines are genuinely interchangeable, not just similar. The frame dimensions, the conveyor height, the sealer belt width and the HMI program are all set to the same values, and the electrical drawings are issued once and applied to both. This matters during the build because a spare part or a setting change that works on one line is guaranteed to work on the other, and it matters after delivery because the customer’s maintenance team only has to learn one set of procedures and hold one common set of spares.
The communication rhythm through the project was deliberately simple. At the build stage we confirmed the blank sample, the carton dimensions and the site voltage in writing before fabrication, so nothing was left to interpret. At the test stage we sent the running videos rather than a written claim, and held crating until the customer’s confirmation came back. The handoff stage is the document pack and the marked cases described above. Keeping these three gates explicit is what lets an order for two machines across two packing areas finish without a round of rework.
Where this layout fits and where it does not
This arrangement suits an operation that runs a limited set of carton formats, wants a person to check the contents of every box, and is losing time to manual erecting and sealing. It is a sensible middle step between a fully manual room and a fully automatic case packer. It is less suited to a plant that runs many carton sizes with frequent switches through the shift, because each format change still means resetting the magazine, rails and sealing width, and to a single-SKU high-volume line where an automatic loading head would remove the manual station as well. For the engineering detail on sizing each station and deciding between automatic and semi-automatic units, see the companion piece on configuring an end-of-line carton packing line.
If you are planning a similar line and want to know what information we need before quoting, start with the carton dimensions and board grade, the target number of sealed cartons per shift, the number of formats and how often you change between them, and the site voltage and frequency. You can send those through the contact page and we will return a layout and a fixed specification.