Yes, unless it is a collaborative robot. Industrial palletizing cells are fenced with light curtains. Budget for it in the cell layout.
Can the robot handle pallets of different heights?
Yes — the controller stores patterns for each case size and pallet height. Recipe changeover is minutes.
Summary
Robotic palletizers for multi-SKU co-packers and mixed lines; conventional layer palletizers for single-SKU high-speed plants; low-level palletizers for small low-speed lines. Size the arm to your heaviest case, spec the gripper for every product you run, and budget the whole cell — collation, pallet dispenser, stretch wrapper and safety fence — not just the robot. Send us your case sizes, line speed and pallet pattern and we will spec the right palletizing cell — and tell you if a cheaper option will do.
Sources
Speed ranges and gripper options referenced: Fanuc, ABB and KUKA palletizing robot application catalogs; Pearson and Columbia conventional layer palletizer literature; PMMI ProSource palletizing machine buyer directory. The Poznan dairy configuration is this project’s own. Speed figures are industry estimates.
Related reading
- Orbital vs turntable stretch wrapper for long profiles
- Open-mouth FFS vs valve bag vs pre-made pouch bagging
Typically 10–40, depending on arm reach and case weight. High-speed lines need a layer palletizer.
Do I need a safety fence?
Yes, unless it is a collaborative robot. Industrial palletizing cells are fenced with light curtains. Budget for it in the cell layout.
Can the robot handle pallets of different heights?
Yes — the controller stores patterns for each case size and pallet height. Recipe changeover is minutes.
Summary
Robotic palletizers for multi-SKU co-packers and mixed lines; conventional layer palletizers for single-SKU high-speed plants; low-level palletizers for small low-speed lines. Size the arm to your heaviest case, spec the gripper for every product you run, and budget the whole cell — collation, pallet dispenser, stretch wrapper and safety fence — not just the robot. Send us your case sizes, line speed and pallet pattern and we will spec the right palletizing cell — and tell you if a cheaper option will do.
Sources
Speed ranges and gripper options referenced: Fanuc, ABB and KUKA palletizing robot application catalogs; Pearson and Columbia conventional layer palletizer literature; PMMI ProSource palletizing machine buyer directory. The Poznan dairy configuration is this project’s own. Speed figures are industry estimates.
Related reading
- Orbital vs turntable stretch wrapper for long profiles
- Open-mouth FFS vs valve bag vs pre-made pouch bagging
Yes, if the lines share a collation conveyor and the robot has enough speed. That is the standard reason to buy a robot instead of two separate palletizers.
How many cases a minute can a robot handle?
Typically 10–40, depending on arm reach and case weight. High-speed lines need a layer palletizer.
Do I need a safety fence?
Yes, unless it is a collaborative robot. Industrial palletizing cells are fenced with light curtains. Budget for it in the cell layout.
Can the robot handle pallets of different heights?
Yes — the controller stores patterns for each case size and pallet height. Recipe changeover is minutes.
Summary
Robotic palletizers for multi-SKU co-packers and mixed lines; conventional layer palletizers for single-SKU high-speed plants; low-level palletizers for small low-speed lines. Size the arm to your heaviest case, spec the gripper for every product you run, and budget the whole cell — collation, pallet dispenser, stretch wrapper and safety fence — not just the robot. Send us your case sizes, line speed and pallet pattern and we will spec the right palletizing cell — and tell you if a cheaper option will do.
Sources
Speed ranges and gripper options referenced: Fanuc, ABB and KUKA palletizing robot application catalogs; Pearson and Columbia conventional layer palletizer literature; PMMI ProSource palletizing machine buyer directory. The Poznan dairy configuration is this project’s own. Speed figures are industry estimates.
Related reading
- Orbital vs turntable stretch wrapper for long profiles
- Open-mouth FFS vs valve bag vs pre-made pouch bagging
SunAura Machinery Specifies a Robotic Palletizer for a Polish Dairy Co-Packer: Why Robot Beat a Conventional Layer Palletizer for Mixed Cases of Yogurt and Cheese
A dairy co-packer in Poznan came to us last month with a room built for a palletizer. They were running yogurt cups and cheese blocks through three filling lines, ending up on three outfeed conveyors, and they needed those cases stacked on pallets for distribution. They asked three suppliers for quotes and got three different machines: a conventional gantry layer palletizer, a robotic arm palletizer, and a low-level case palletizer. We specified the robotic arm. This article explains why — and when a conventional layer palletizer still wins.
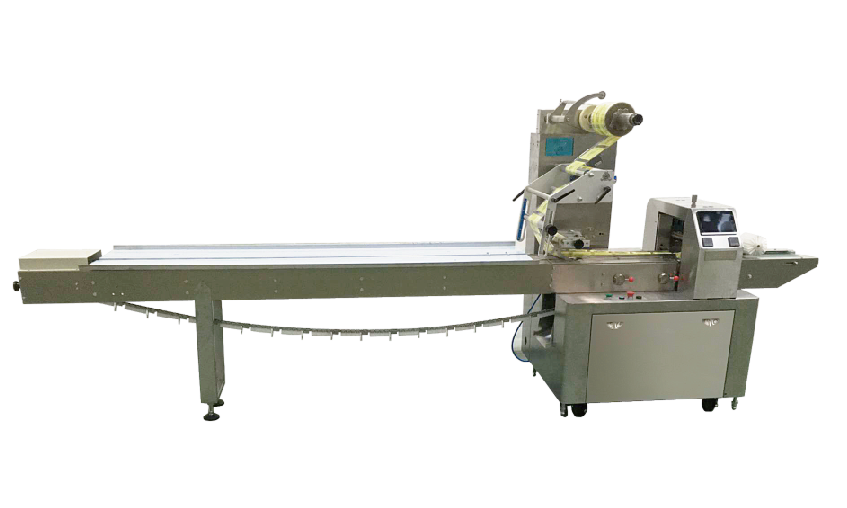
The three ways to palletize cases
A conventional layer (gantry) palletizer uses a hoist that lowers a layer plate onto a stack, pushes a full layer of cases across onto the pallet, and repeats. It is the workhorse of the end-of-line and runs 40–60 cases a minute. A robotic palletizer uses a 4- or 6-axis arm with a vacuum or gripper end-of-arm tool, picking one or two cases at a time and placing them on the pallet in a pre-programmed pattern. A low-level (semi-automatic) palletizer is a compact machine that picks cases at floor level; it is slower and cheaper. All three end up with a wrapped pallet. They differ in speed, product mix, footprint and price.
| Robotic arm palletizer | Conventional layer palletizer | Low-level palletizer | |
|---|---|---|---|
| Speed | 10–40 cases/min | 40–80 cases/min | 5–15 cases/min |
| Mixed SKUs | Excellent | Poor (one pattern) | Good |
| Floor space | Compact | Large, high | Small |
| Changeover | Recipe-driven, minutes | Mechanical, hours | Manual |
| Relative cost | Medium–high | High | Low |
| Best for | Multi-SKU co-packers | Single-SKU high-speed | Small plants, low speed |
Why the robot won in Poznan
The dairy was running yogurt cups in 12-count cases, cheese blocks in 6-count cases, and butter bricks in 24-count cases — three different case sizes on three outfeeds, changing over twice a shift. A conventional layer palletizer is built for one case pattern and one line; changeover takes hours and needs a mechanic. A robotic arm stores every pattern in its controller and switches between them in minutes. The robot also handles the collation conveyor from three lines without a massive gantry structure. We paired the robot with a vacuum gripper that handles both RSC cases and shrink-wrapped trays, and an inline stretch wrapper downstream. The dairy got one palletizer for three lines, which was the economic answer.
When a conventional layer palletizer is the right call
If you run one product, one case size, 24 hours a day — a bottled water line, a brewery, a canned food factory — the conventional layer palletizer is still the standard. It runs faster (60–80 CPM), it is simpler to maintain for a plant mechanic, and it handles very heavy cases. A robotic arm at 40 CPM cannot keep up with a 60 CPM high-speed line. For a single-SKU high-speed plant, the layer palletizer wins on speed and cost per case. SunAura builds both; we will not push a robot on a water bottler who needs speed.
What the robotic palletizer cannot do
Do not buy a robot for a 60 CPM single-SKU line — it is too slow. Do not buy it for extremely heavy loads (over 30 kg per case) without checking the arm payload; a 50 kg case needs a heavier and more expensive arm. And do not forget the infeed collation: a robot needs cases queued and presented in a known position. Without an accumulation and collation conveyor, the robot waits idle. SunAura designs the collation, the pallet dispenser, and the outfeed stretch wrapper as one cell.
End-of-arm tool: vacuum vs fork vs clamp
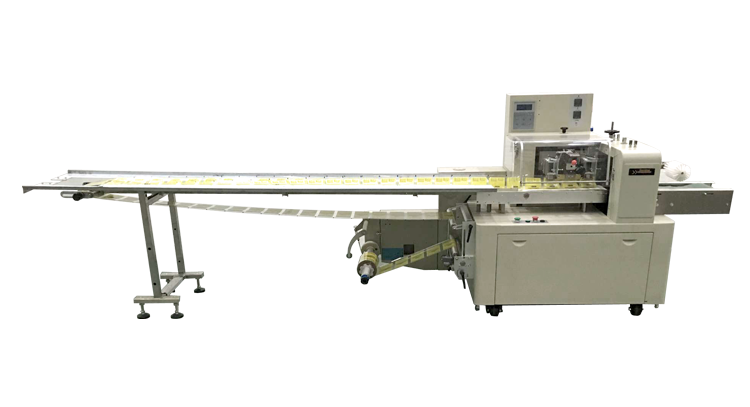
The gripper defines what the robot can pick. Vacuum grips corrugated cases and shrink-wrapped trays. Forks slip under the pallet or layer. Clamps squeeze the case sides. A dairy line running both RSC cases and shrink-wrapped trays needs a dual gripper or an automatic tool changer. Specify the tool based on every product you run, not just the headline product. A vacuum tool on a leaky shrink-wrapped tray drops the load. Ask for the tool change time and whether spare tools are included.
Integration with the upstream line
A palletizer is the last station on the line. It has to talk to the upstream case erector, the case packer, and the outfeed conveyor. For a three-line dairy, the robot’s controller needs signals from all three lines so it knows which case is coming. SunAura integrates the palletizer into the line PLC so collation and robot motion are synchronized. A palletizer bought as a separate bolt-on often misses this integration and jams when two lines send cases at once.
Pallet dispenser and stretch wrapping
The palletizer is not a complete cell. You also need: an empty pallet dispenser (magazine), a layer sheet dispenser (if you use tier sheets), and a stretch wrapper downstream. The robot places cases; the wrapper secures the load. For a dairy distribution center, a turntable stretch wrapper is standard. Ask for the whole cell price, not just the robot. A robot without a pallet dispenser is a mechanical arm sitting on the floor.
Safety fencing and cell layout
An industrial palletizing robot is a fenced cell. The layout matters: the robot needs a clear work envelope, the collation conveyor enters from one side, the pallet dispenser feeds empty pallets, and the stretch wrapper takes the loaded pallet out the other. Safety fencing with light curtains and interlocked gates is required. For a dairy plant with washdown, the cell needs stainless or painted steel that can be hosed down. Plan the cell footprint before you order — a robot that does not fit through the factory door is a classic installation delay. SunAura does a site survey before quoting the cell layout.
Pallet patterns and layer sheets
The robot stores pallet patterns in its controller. For a dairy with three case sizes, three patterns are stored. When a new case size comes, the robot learns the pattern by walking through it once. Layer sheets (slip sheets between layers) are optional but recommended for unstable loads. A sheet dispenser places a thin cardboard or plastic sheet between layers. For yogurt cups that shift, layer sheets prevent the top layer from sliding. For rigid cheese blocks, they are optional. Specify the sheet dispenser if your loads are unstable.
Robot payload and reach: sizing the arm
Pick the robot arm based on the heaviest case plus the gripper weight, and the longest reach needed. A 20 kg case with a 10 kg vacuum gripper needs a 35–40 kg payload arm. A 5 kg case with a small gripper fits a 20 kg arm. Under-sizing the payload is a common mistake — the robot slows down and overheats. Reach is equally important: the arm has to cover the collation conveyor, the empty pallet position, and the stretch wrapper outfeed in one envelope. SunAura sizes the arm after a site survey. A robot bought on brochure dimensions often does not reach the stretch wrapper.
Maintenance and spare parts
Robotic arms are low-maintenance: the gearbox is sealed, the motors are brushless. The wear parts are the gripper pads, the vacuum cups, and the safety light curtains. Keep spare cups and pads on the shelf. A conventional layer palletizer has more mechanical wear: chains, bearings, push bars, and hoist brakes. For a plant with one maintenance person, the robot is easier. For a plant that runs 24/7, both need a preventive maintenance schedule. Ask the supplier for the recommended PM interval and the cost of wear parts. SunAura ships the spare parts list with the cell.
Payback and ROI
A robotic palletizer replaces one or two manual palletizer operators per shift. On a two-shift plant, that is 3–4 operator wages. On a three-shift plant, 5–6. The machine pays back in 18–30 months on labor alone, before counting reduced worker’s comp claims and pallet load consistency. A conventional layer palletizer replaces two operators but costs more upfront and only works on a single line. For a co-packer with multiple lines, the robot’s multi-line capability shortens the payback. SunAura runs the payback numbers with your labor cost before quoting.
FAT, installation and training
Before the cell ships, ask for a Factory Acceptance Test with your own cases and pallets. The FAT proves the robot picks your actual cases, builds your patterns, and the stretch wrapper secures your load. On-site installation takes 1–2 weeks: anchor the cell, run utilities, integrate with upstream lines, and train operators. A co-packer that runs multiple shifts needs at least two operators trained on the robot controller. SunAura includes FAT and operator training in the cell price.
What not to buy
Do not buy a robotic palletizer for a single-SKU high-speed line. Do not buy it without the infeed collation and pallet dispenser. Do not forget the stretch wrapper. And do not under-specify the gripper — a tool that drops cases on the floor every shift will destroy the ROI. SunAura quotes the complete palletizing cell: robot, gripper, collation, pallet dispenser, stretch wrapper and controls.
Budgeting the palletizing cell
A robotic palletizing cell is a mid-range capital purchase. The robot arm is the headline, but the gripper, safety fencing, collation conveyor, pallet dispenser and stretch wrapper add up. Compare fully-installed cell prices across suppliers, not just the robot model. A cell that replaces two manual palletizers pays back in 18–30 months on labor alone. A cell that replaces one layer palletizer on a single-SKU line usually does not — that is why we specify layer palletizers for those plants.
FAQ
Can one robot handle two lines?
Yes, if the lines share a collation conveyor and the robot has enough speed. That is the standard reason to buy a robot instead of two separate palletizers.
How many cases a minute can a robot handle?
Typically 10–40, depending on arm reach and case weight. High-speed lines need a layer palletizer.
Do I need a safety fence?
Yes, unless it is a collaborative robot. Industrial palletizing cells are fenced with light curtains. Budget for it in the cell layout.
Can the robot handle pallets of different heights?
Yes — the controller stores patterns for each case size and pallet height. Recipe changeover is minutes.
Summary
Robotic palletizers for multi-SKU co-packers and mixed lines; conventional layer palletizers for single-SKU high-speed plants; low-level palletizers for small low-speed lines. Size the arm to your heaviest case, spec the gripper for every product you run, and budget the whole cell — collation, pallet dispenser, stretch wrapper and safety fence — not just the robot. Send us your case sizes, line speed and pallet pattern and we will spec the right palletizing cell — and tell you if a cheaper option will do.
Sources
Speed ranges and gripper options referenced: Fanuc, ABB and KUKA palletizing robot application catalogs; Pearson and Columbia conventional layer palletizer literature; PMMI ProSource palletizing machine buyer directory. The Poznan dairy configuration is this project’s own. Speed figures are industry estimates.