Why a Beverage Canner Chose On-Site Nitrogen Generation Over Delivered Gas for Purging
A craft-to-mid-size beverage canner running carbonated drinks and nitrogen-flushed still products found itself paying closer attention to a line item that had quietly grown: the gas bill. Every can receives a measured dose of liquid nitrogen immediately before the lid is seamed, which both displaces oxygen to protect flavour and builds the internal pressure that stops a thin aluminium can from collapsing. The process was working, but the nitrogen arrived in delivered containers, and the invoices were carrying more than the cost of the gas itself. This is the story of why the plant moved to on-site nitrogen generation, how it chose between the two generator technologies, and where delivered gas remains the genuinely better answer rather than something to be replaced on principle.
At SunAura Machinery we integrate filling, seaming and packaging lines that use inert gas, and the honest framing is that the gas supply is a utility decision rather than a packaging-machine decision. It changes nothing about the can or the seam, but it changes the operating cost, the supply risk and the capital profile of the whole line, which is exactly why it deserves a proper comparison rather than a default.
What Delivered Gas Actually Costs
The plant had two delivered options on the table and had used both at different times. Compressed gas cylinders store a large volume at high pressure, around 300 bar, and are simple to install with no upfront capital. They are a sensible answer for low consumption and for covering occasional peaks, but they are bulky and heavy to handle, the unit price is high because production and delivery are built in, and the operation depends on the supplier’s rack and delivery schedule. At the canner’s volume, cylinders meant constant changeovers, storage space for full and empty racks, and the safety burden of moving high-pressure steel around a busy line.
The larger delivered option is bulk liquid nitrogen, held in an insulated tank and vaporized on site, with the cryogenic liquid delivered by insulated tanker. It is cheaper per unit than cylinders and handles high consumption well, but it brings a different set of commitments. The tank typically sits under a multi-year contract, commonly five to seven years, needs a dedicated foundation and evaporator, and the insulation is imperfect: when consumption is low, the liquid warms and vents to atmosphere as boil-off, which industry sources put as high as roughly one percent of the remaining tank volume per day, with tanks typically refilled weekly. At minus 196 degrees Celsius, the liquid also carries a real frostbite and handling risk. For a plant whose demand was steady but not enormous, the combination of long contract, boil-off and delivery dependence was the prompt to look at making the gas on site.
On-Site Generation: Membrane and PSA
On-site generators do not use cryogenic distillation at all. They take a stream of clean, dry compressed air and separate the nitrogen from it, so the plant owns its own continuous supply with no tanker and no cylinder handling. The two technologies achieve this differently. A membrane generator pushes compressed air through bundles of hollow polymer fibres; oxygen, water vapour and other gases permeate through the fibre walls while nitrogen travels through and is collected. It has almost no moving parts, starts producing gas in seconds, runs very quietly and tolerates higher ambient temperatures well. A pressure swing adsorption, or PSA, generator instead passes air through columns filled with carbon molecular sieve that adsorbs oxygen under pressure, cycling two vessels so one is producing while the other regenerates. It achieves higher purity and higher efficiency, at the cost of a slightly larger footprint, a startup measured in minutes rather than seconds, and periodic blow-off noise.
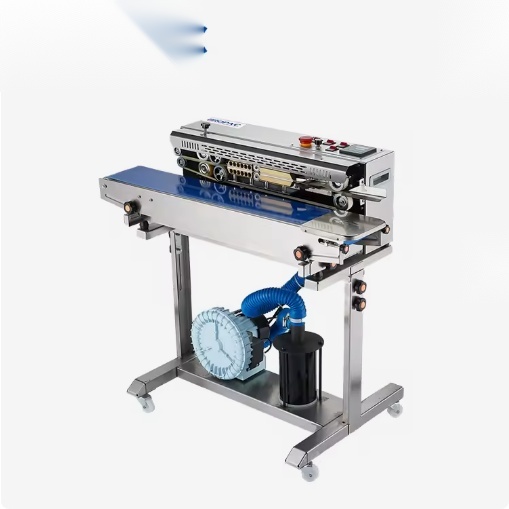
Both technologies need the same disciplined inputs. The feed air must be dry and essentially free of liquid water and oil, typically below a hundredth of a milligram per cubic metre, so the generator sits behind proper filtration and drying. Neither method reaches cryogenic purity for free — pushing the purity higher costs more compressed air and therefore more energy, and the key design principle is to produce the purity the application actually needs rather than the highest number available. Industry sources put membrane purity up to roughly 99.9 percent and PSA up to around 99.999 percent, which is more than enough headroom for food and beverage purging, where the required purity is usually well below the pharmaceutical extreme.
Selection Table: Nitrogen Supply Options Side by Side
| Dimension | Cylinders | Bulk liquid | Membrane generator | PSA generator |
|---|---|---|---|---|
| Upfront capital | None | Low; tank often rented | Mid | Mid to high |
| Unit cost of gas | Highest | Lower than cylinders | Low; mainly electricity | Lowest at high purity |
| Typical purity | Fixed high | Fixed cryogenic high | Up to ~99.9% | Up to ~99.999% |
| Startup / readiness | Immediate | Immediate after install | Seconds | Minutes |
| Supply risk | High; delivery dependent | High; tanker and contract | Low; self-produced | Low; self-produced |
| Storage loss | Minimal | Boil-off, up to ~1%/day | None; make on demand | None; make on demand |
| Peak demand | Handles peaks well | Handles peaks | Needs buffer tank | Needs buffer tank |
| Main weakness | Handling, cost, changeovers | Long contract, boil-off, frostbite risk | Purity ceiling and air quality needs | Footprint, blow-off noise |
When On-Site Generation Wins — and When It Does Not
Choose on-site generation when nitrogen use is continuous and substantial enough that the avoided delivery, rental and boil-off charges cover the capital, and when supply independence matters to the operation. The canner’s steady shift pattern and the cost of a stopped seaming line made self-supply attractive, and the ability to size purity to the actual purging requirement meant it was not paying for cryogenic-grade gas it never needed. Between the two generators, membrane is the natural fit for moderate purity, a small footprint, fast startup and a warm plant environment, while PSA is the better choice when the process needs higher purity, runs long hours and benefits from the higher efficiency at that level.
Do not assume generation is always better. At genuinely low or intermittent consumption, cylinders remain the rational choice because there is no capital sitting idle and no compressor running for a few doses a week. Where a bulk tank is already in place under a favourable contract and the plant is close to a reliable gas source, switching early can mean paying to break an agreement to solve a problem that does not exist. On-site generators also shift the burden onto your compressed-air system: if the existing compressor is undersized, unreliable or poorly maintained, the generator inherits that weakness, and the project should include the air treatment and a buffer tank rather than treating them as optional. The honest recommendation is to model the real delivered cost — including the rental, delivery and boil-off that never appear in the headline gas price — against the capital and the energy, and let that comparison decide rather than the appeal of energy independence.
Purity, Sizing and the Buffer Question
The single most common sizing error is over-specifying purity. Because every extra point of purity costs compressed air and energy, producing 99.999 percent gas for a can-purging duty that is comfortably served at a much lower level is a permanent, invisible operating cost. The correct method is to establish the residual oxygen or purity target from the process — the shelf-life and pressure requirements — and size the generator to that, with margin, rather than to the highest available figure. A short trial with residual-oxygen measurement on the actual product is far more reliable than a generic specification.
Generators are sized for average flow, but a packaging line takes gas in short bursts at the dosing and flushing points, which is why a buffer or receiver tank is not an optional extra. It stores gas so the generator runs at a steady rate while the line draws peaks, and it provides a reserve for short high-demand periods. Sizing the buffer against the real burst profile — number of cans per minute, dose volume and any simultaneous flushing stations — is what prevents pressure dips that would otherwise produce inconsistent dosing and out-of-spec cans.
Cost, Payback and Procurement Risks
The payback is built from the difference between the delivered all-in cost and the cost of self-produced gas. On the delivered side, the real figure is not just the gas price per cubic metre but cylinder rental and handling, delivery and administration charges, and the boil-off that vents unused bulk liquid to atmosphere. On the generated side, the cost is largely the electricity for the compressor and generator plus routine maintenance and filter changes, with no logistics margin and no storage loss. Plants with steady, high utilization typically reach payback in a few years and then run at a stable unit cost, insulated from gas-price increases and delivery disruption; the exact period depends on local electricity prices and the delivered contract being replaced, so it should be calculated rather than assumed.
The procurement risks are concentrated in the supporting systems. The liquid filling machines and the dosing station need a stable gas pressure, which the conveyors and line layout and the form-fill-seal packaging machines also rely on, so the generator, compressor, dryer and buffer have to be sized as one utility system rather than bought separately on price. Confirm the compressed-air capacity exists before committing, specify the air quality instrumentation, and include the maintenance contract and filter schedule; a generator starved of clean, dry air fails slowly and unpredictably, and the fault will look like a packaging problem rather than a utility one.
Frequently Asked Questions
Membrane or PSA — which generator should a beverage plant choose?
For moderate purity, a compact footprint, fast startup and a warm plant, membrane is the simpler fit. For higher purity, long running hours and the best efficiency at that level, PSA is the stronger choice. The decision should follow the purity target the process actually needs rather than the technology preference.
Will an on-site generator keep up with a high-speed canning line?
Yes, when the generator is sized for average flow with a correctly sized buffer tank that absorbs the dosing bursts. The tank is the critical component for matching steady production to a bursty line demand, so it should be calculated from the real dose volume and cans per minute.
Is self-produced gas really cheaper than bulk liquid?
At steady, high utilization it usually is, because there is no delivery margin, rental or boil-off, and the cost is mainly electricity. At low or intermittent use, delivered gas can remain cheaper because no capital is sitting idle, which is why the all-in delivered cost should be modelled before deciding.
What happens if the generator or compressor stops?
The buffer provides a short reserve, and many plants keep a small delivered backup for a prolonged outage. A preventive maintenance schedule and monitoring of air quality and pressure give early warning, so a utility fault does not become an unplanned line stop.
Summary: Produce the Purity You Actually Need
The canner’s decision came down to total cost and supply independence. Cylinders are simple but carry the highest unit cost and constant handling; bulk liquid is cheaper yet locks the plant into long contracts and loses up to roughly one percent a day to boil-off. On-site membrane and PSA generators make gas on demand from clean compressed air, with no delivery, no storage loss and an adjustable purity that should be matched to the process rather than maximized. Choose membrane for moderate purity and fast startup, PSA for higher purity and long hours, and always size the buffer to the burst profile. Keep delivered gas for low or intermittent use and for sites where a favourable contract already exists, and do not move generation onto a compressor that cannot support it. Done right, the line runs on a stable, self-owned gas supply and the old delivery invoice becomes a cost it no longer carries.
Sources and Further Reading
- Atlas Copco Compressed Air Wiki, Choosing the Right Nitrogen Supply for Your Business, covering cylinders, bulk liquid, membrane and PSA, including boil-off, contract and purity figures.
- Industry nitrogen generation literature on membrane and pressure swing adsorption total lifecycle cost and the hidden charges in delivered gas (rental, delivery, administration and boil-off).
If you are weighing delivered gas against on-site generation, our utility and applications team can model the all-in cost, purity target and buffer sizing against your real canning throughput. The same process discipline runs through our guide to robotic end-of-arm tooling, and for the quality checks that protect every sealed pack, see how vacuum decay leak testing catches weak seals before they ship. Share your current gas invoices and line burst data and we will recommend the generator, air treatment and backup plan — contact SunAura Machinery to run the comparison.