
What Is Induction Sealing and Why Does It Matter?
Walk a bottling line after a long August shift and you’ll find it on the returns pallet: a few hundred PET bottles leaking through the cap, product weeping down the thread. The cap torque reads fine. The liner is sitting inside the cap exactly where it should. So where is the failure? Almost always, the bottle cap sealing step on that line was never actually creating a hermetic barrier — it was just squeezing a foam disc flat. If you’ve ever asked how induction sealing works on a line like yours, the short answer is that it bonds a foil disc straight to the rim, and it’s one of the cheapest, highest-return upgrades a liquid or powder filling line can make.
Induction sealing is a non-contact method that bonds a thin aluminum foil laminate directly to the rim of a plastic (or specially coated glass) bottle mouth after the cap is applied. The cap still does its regular job — keeping dust out, holding dust caps, providing grip — but the foil disc becomes the real barrier between product and outside world. Once it’s sealed, the bottle is hermetic: no leak path, no wicking, no oxygen migration. And the first person to twist the cap sees a popped, breached foil, which is what gives you tamper-evidence that a simple liner can’t fake.
A hermetic seal you can’t fake
A pressure-sensitive liner and a cap torque set to spec will slow evaporation for a while. They won’t stop liquid wicking past the thread under vibration. We saw a pharmaceutical manufacturer in Jiangsu losing roughly 3% of bottled product to cap leakage before switching to induction sealing — mostly syrups and suspensions wicking past the thread over a six-month shelf life. That 3% sounds small until you annualize it across a 6,000-bottle-per-hour line. The hermetic seal for food packaging and pharma applications is a regulatory expectation as much as a technical one: once foil is fused to the rim, the bottle will bulge on its own before it leaks through the seal.
Where it shows up on the production line
You’ll find it on cooking oil bottles, peanut butter jars, pharmaceutical syrups and tablets, agrochemicals, cosmetics and motor oil — any bottled product that stacks on a pallet. The aluminum foil sealing step sits after capping and before date coding, so it rarely forces a line redesign. Most customers add the sealer over a weekend and run product Monday morning.
The Physics: How Electromagnetic Induction Creates a Hermetic Seal
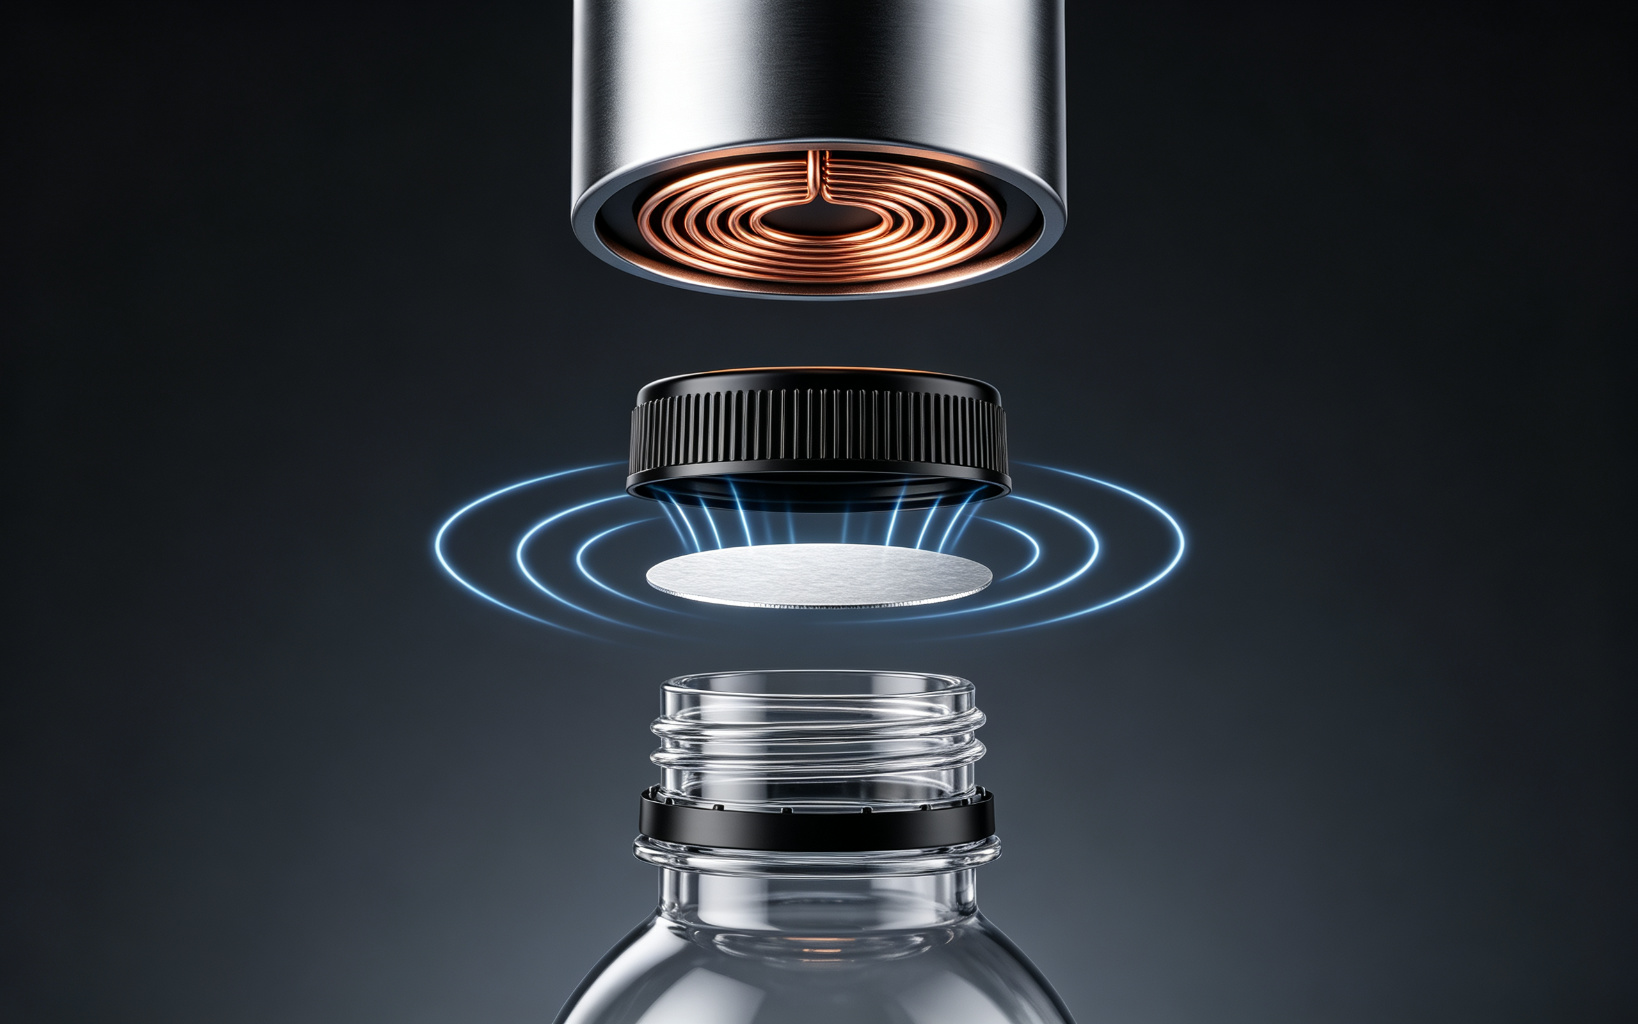
Here’s what actually happens on the factory floor. The sealing head contains a coil of copper tubing fed by a high-frequency power supply, typically 20–100 kHz. When a capped bottle passes under the coil, the alternating current generates an alternating magnetic field that couples through the cap plastic straight into the thin aluminum disc inside. The aluminum is conductive, so the field induces circulating currents in the foil — eddy currents. Those currents meet the resistance of the aluminum, which converts energy into heat, exactly how an induction cooktop heats a pan without touching it.
Eddy currents and the foil laminate stack
The liner inside the cap isn’t a single sheet. It’s a laminate, usually a three-layer sandwich: a PET (or foam) top layer that protects the foil, a thin pure aluminum foil in the middle that does the heating, and a heat-sealable PE layer on the bottom that touches the bottle rim. The eddy currents heat the aluminum in roughly 0.5–2 seconds. That heat melts the bottom PE layer, which flows and wets the bottle rim while the cap holds it down. Once the bottle leaves the field, the PE cools and solidifies, gluing the foil disc to the rim. This stack is what makes aluminum foil sealing work on non-conductive plastic: the plastic itself never heats up, only the foil does, which is why you can seal a thin PET bottle without deforming the thread.
Why it only takes a second
Total dwell time is short. On a 28–38 mm neck PET bottle running 1,000–2,000 bottles/hour, the coil energizes for 0.3–0.8 seconds. At a 200 mm jar diameter — a gallon of oil or a large supplement tub — sealing time typically runs 1.5–2.5 seconds, because there’s more foil area to heat and more rim to wet. The machine never touches the cap. That’s the point of electromagnetic induction: heat is generated inside the foil itself, contact-free, with no wearing seals and nothing to clean between runs. If you want the deeper materials-science write-up, Packaging World runs a solid technical archive on liner design and coil geometry at packworld.com.
Anatomy of an Induction Sealing Machine
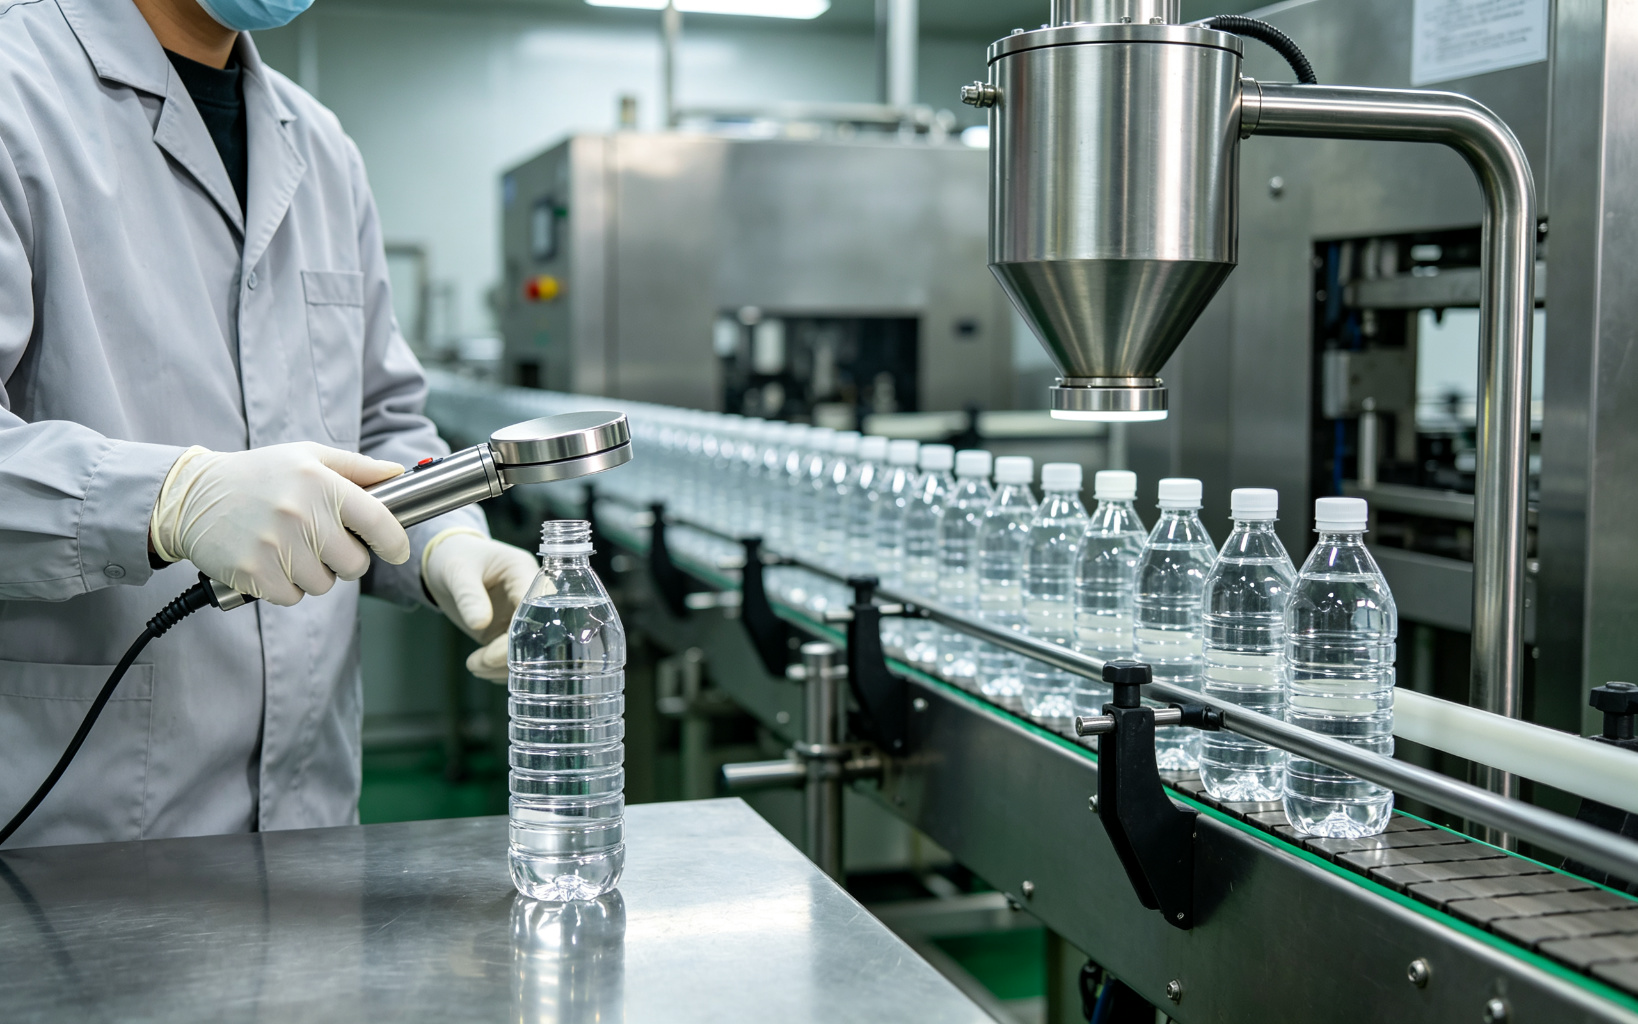
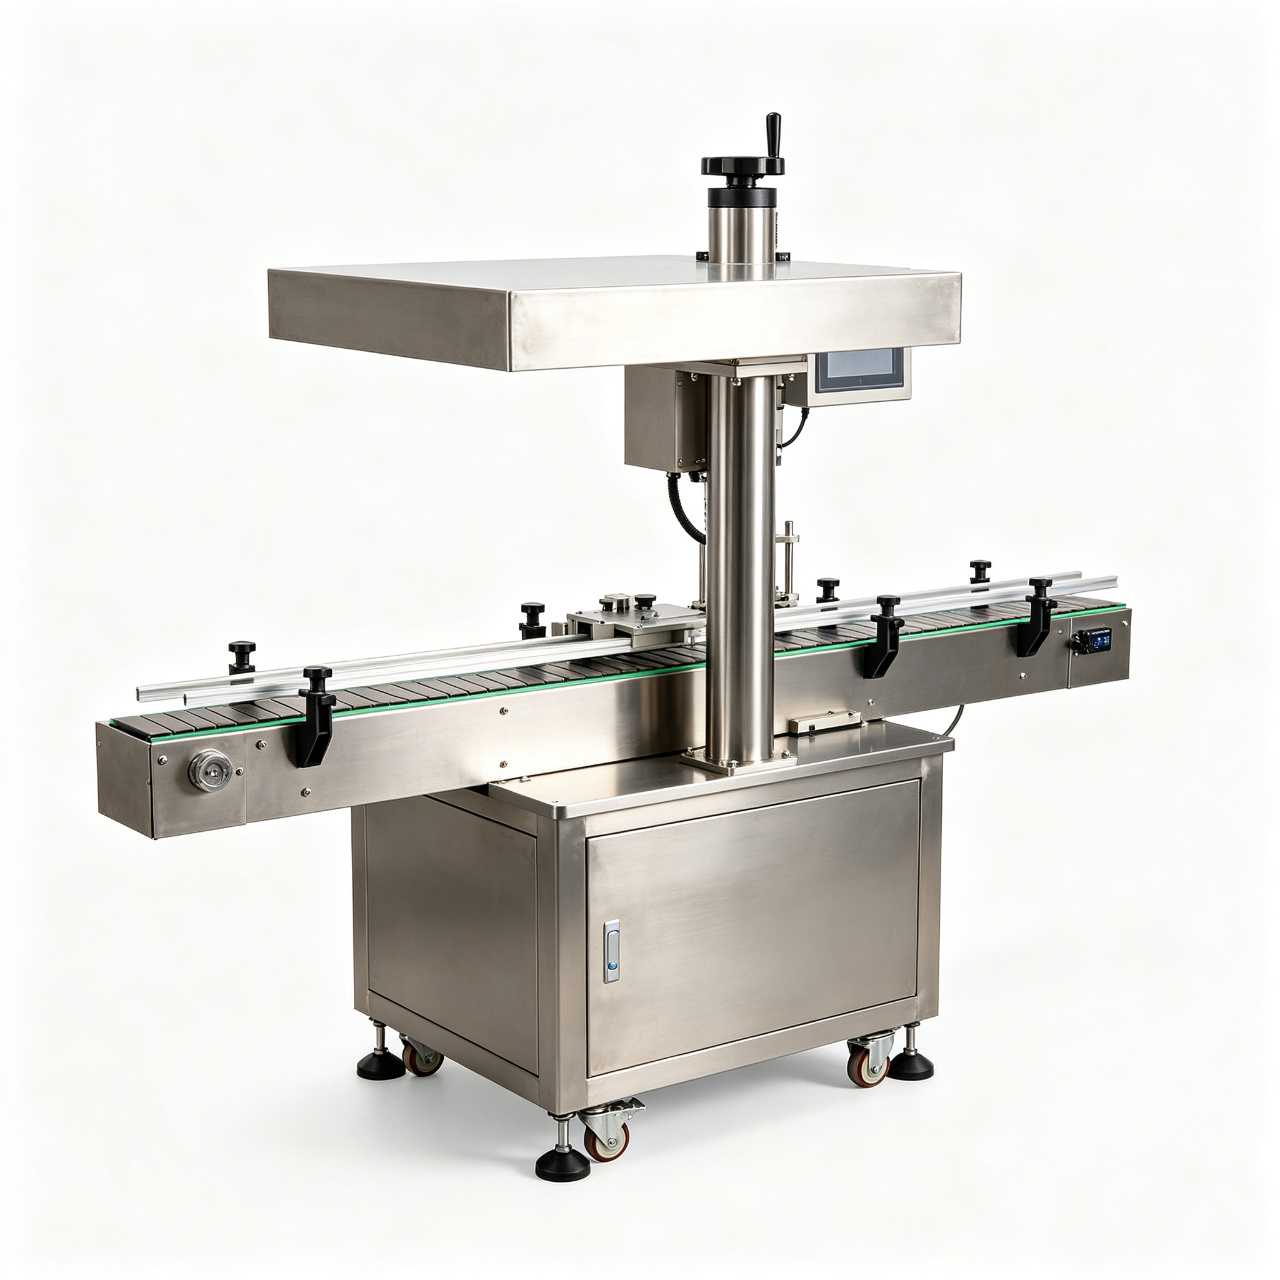
An industrial induction sealing machine has four basic blocks: a high-frequency generator (the power supply), a copper induction coil formed to your cap diameter, a conveyor or indexing mechanism that brings each bottle under the coil, and a controller that sets power, time and head gap. The differences between models are almost all about throughput and how the bottle gets to the coil. SUNAURA builds both continuous and handheld platforms on the same generator electronics, which makes field upgrades straightforward if a line grows.
Continuous inline systems
Continuous induction sealers mount over an existing conveyor. Bottles pass under a ring or flat coil at line speed while the generator runs continuously — no start/stop per bottle. Power output ranges 1–5 kW for typical continuous models, with high-power units (5–10 kW+) reserved for large jars, thick-wall containers or fast lines above 200 BPM. These are what you bolt onto a filling line that’s already running. Pair them with our conveyor solutions that give you straight, stable, centered travel under the coil — a bottle that wanders laterally under the seal head is a bottle that gets a half-sealed rim. You can browse the full induction sealing machines range on our product page, including the PET bottle induction sealer configured for 28–89 mm caps.
Handheld and bench-top units
A handheld induction sealer is a wand: you hold the sealing tip over a capped bottle, pull the trigger, and the coil energizes for a fixed timer. Power is usually 0.5–2 kW, throughput a few hundred to maybe 1,000 bottles per shift, and the operator moves bottle to bottle. These suit R&D labs, short runs, contract packing, or lines under ~30 BPM. They’re also the right tool if you only need an induction sealing machine for pharmaceutical bottles in a small-fill GMP room and can’t justify a full conveyor, or if you’re sealing a co-packer’s occasional SKU that doesn’t merit inline hardware.
| Parameter | Continuous inline sealer | Handheld / bench-top sealer |
|---|---|---|
| Typical power output | 1–5 kW (up to 10 kW+ for large jars) | 0.5–2 kW |
| Realistic throughput | 30–300+ bottles/min, matched to line speed | ~10–40 bottles/min, operator-dependent |
| Cap / neck range | 20–200 mm, coil swapped per SKU | 20–100 mm with interchangeable tips |
| Line integration | Mounts over existing conveyor; needs centered travel | Bench-top, no integration needed |
| Best fit | Steady runs: food, pharma, chemicals | R&D, short runs, pilot batches |
| Consistency | Repeatable power/time on every bottle | Dependent on operator placement and dwell |
Critical Parameters: Power, Time, and Bottle Material
Most engineers miss this on the first run. They crank the power to max, hit go, and wonder why the seal is either weak (peels off in sheets) or blown (foil melted through, cap top warped). Three numbers decide the result: coil power, dwell time, and the gap between the coil face and the cap top. Get any one of them off and the other two won’t save you.
Power output and gap settings
The starting rule is low and slow. For a standard 28 mm PET cap, a 1.5 kW continuous sealer running at 40–60% power for 0.4–0.6 seconds usually lands in a good window. Set the gap between 3 and 5 mm — too close and you risk arcing and overheating the cap top; too far and the field couples weakly and the seal runs cold. Induction sealing temperature settings aren’t entered directly on the HMI; you set power and time, and the PE layer tells you (by peeling cleanly) whether the liner interface hit 130–180 °C. Build a small DOE — power 40/50/60%, time 0.4/0.5/0.6 s — peel-test five seals per combo, and you’re done inside a half-hour.
When PET, HDPE and glass behave differently
PET seals cleanly because its surface energy is high and it wets molten PE well. HDPE is more slippery and needs a slightly hotter, slightly longer dwell — otherwise the foil peels off in sheets with a shiny, un-wetted rim. PP sits in between. Glass won’t bond to standard PE at all; on glass jars you need a foil liner with a special heat-seal lacquer layer matched to the glass composition, and line speed usually drops because the glass mass draws heat away. If you’re switching resin between product runs, re-run your seal development rather than trusting the old recipe. For pharma lines, keep your seal validation records aligned with ISO 11607 sterile barrier expectations, and confirm liner materials meet FDA food-contact packaging guidance for whatever product you run.
Common Sealing Defects and How to Fix Them
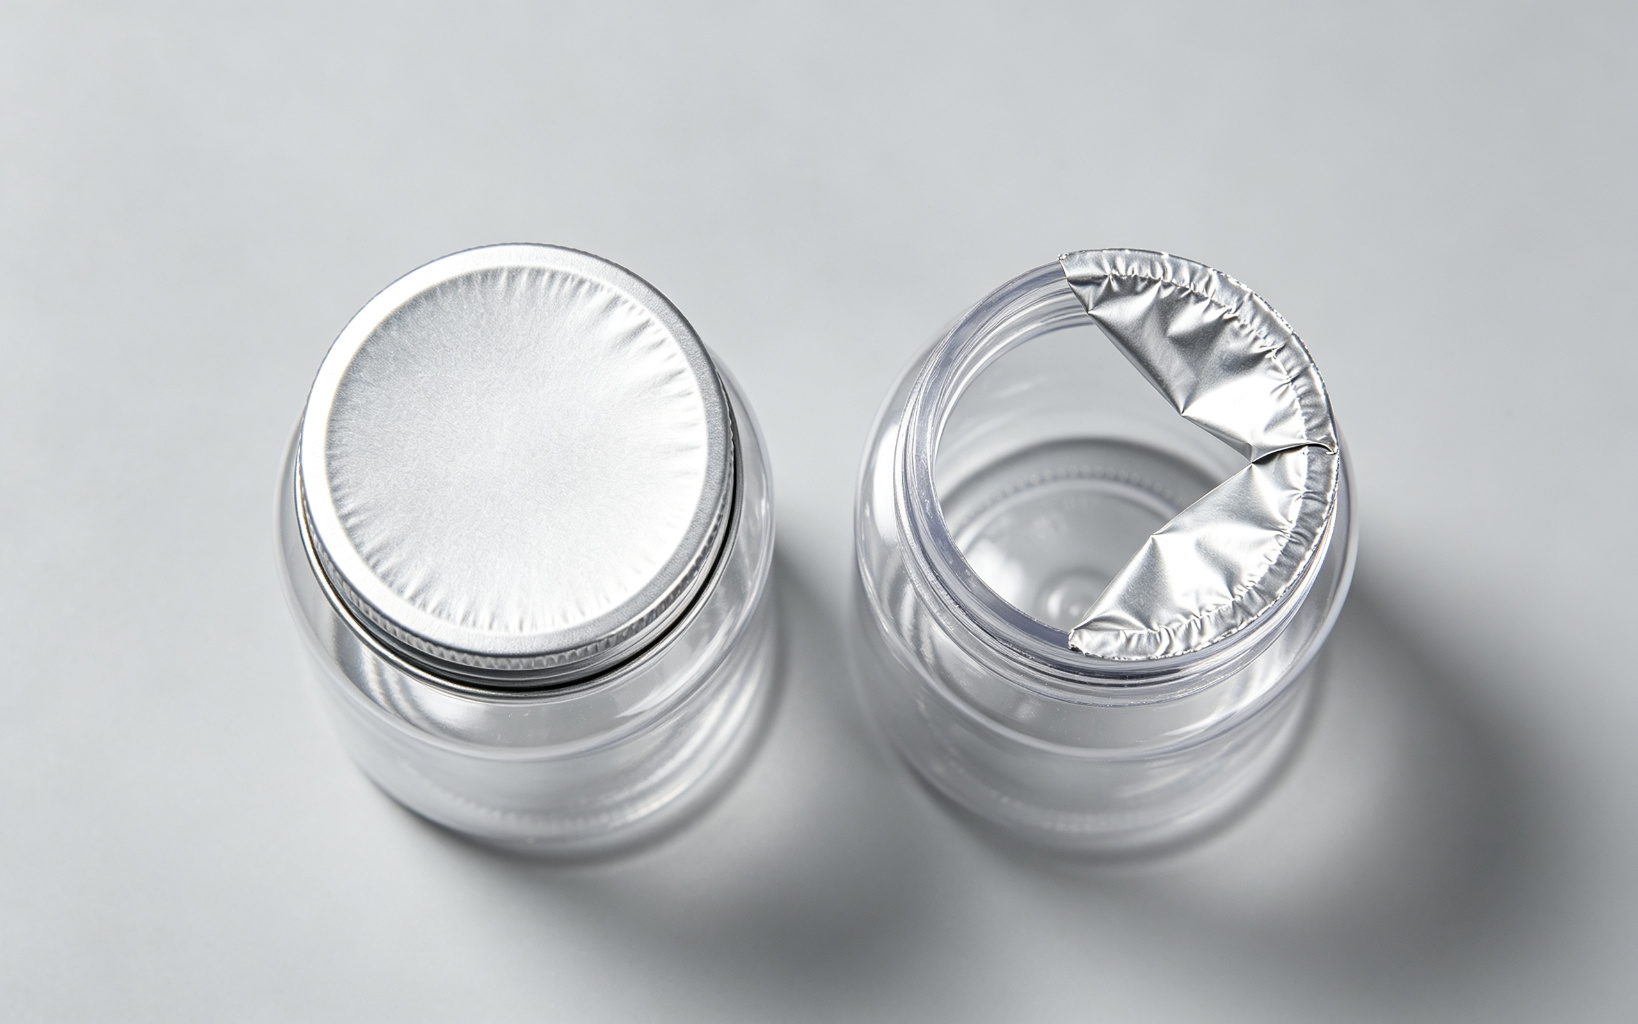
The tricky part is that a lot of defects look like “bad liners” when they’re actually a setup problem. Pull ten bad seals off your reject bin and you’ll usually find one root cause, not ten. Where people go wrong is blaming the liner supplier before checking power, gap, and cap torque.
| Defect | Likely cause | Fix |
|---|---|---|
| Foil peels off cleanly, rim untouched | Under-powered or too short dwell; cap torque too low so liner floats above rim | Raise power 10–15% or add 0.1 s; set cap torque to 8–15 in-lb for 28 mm caps |
| Wrinkled or partial seal around rim | Bottle wandering on conveyor; cap off-center; coil gap uneven | Re-guide conveyor, recenter coil, check star wheel spacing |
| Cap top discolored / foil burned through | Over-powered; gap too small; coil too close to cap | Drop power 10–15%, raise gap to 4–5 mm, shorten dwell |
| Seal looks fine but leaks on drop test | Liner PE resin wrong for your bottle; cold product chilling the rim | Match liner grade to bottle resin; pre-warm product or slow the line |
| Random seals good, random bad | Line voltage sag; loose coil lead; bottle height variation | Check mains stabilizer and coil cable torque; verify neck height consistency |
Frequently Asked Questions
How do I choose between a continuous induction sealer vs handheld?
Run the math on bottles per hour. If your line holds steady at 30 BPM or more for a full shift, go continuous — the payback on leak reduction usually comes inside six months. If you’re sealing under ~1,000 bottles a day, running short SKUs, or validating a new product in R&D, a handheld wand pays for itself in a weekend and can always be retired to lab duty later.
What induction sealing temperature settings should I start with?
You don’t set temperature directly. You set output power (usually 40–70% on a 1.5 kW unit for 28 mm caps) and dwell time (0.3–0.8 s). The liner interface typically reaches 130–180 °C, which is enough to melt the PE seal layer without softening the PET. Confirm the result with a peel test, not a thermometer — a clean peel that leaves a continuous film of PE on the rim is your real target.
Can I induction seal glass bottles?
Yes, but not with a standard PET liner. Glass needs a foil liner with a heat-seal lacquer formulated for glass, and you’ll usually run 20–40% more dwell time because the glass mass draws heat away from the rim. Expect to slow the line slightly. HDPE and PP jars are easier — just confirm the liner grade matches the resin.
How do I verify the seal is actually hermetic?
Three cheap checks cover 95% of the job: visual peel test (foil must come off in one disc with PE fully wetted to the rim), a vacuum or pressure decay test on a sample of bottles, and a drop test from 1.2 m onto a concrete floor. For pharma, log every batch’s power and time settings so you have the validation trail regulators expect. If a bottle passes all three, it’s hermetic.
Next Step: Size Your Induction Sealer With Our Engineers
If you’re sizing an industrial induction sealing machine for your line, our engineers can walk you through the math. Send us your bottle specs — neck diameter, resin, cap type, target bottles per minute, and product temperature — and we’ll come back with a recommended model, a starting power/time recipe, and a realistic SUNAURA induction sealer price before you buy induction sealer hardware. Every unit is built in our 48,000 m² Qingdao plant, CE and ISO 9001 certified, run-tested 48 continuous hours before shipment, and backed by a 12-month warranty. Drop your specs to [email protected] and we’ll reply within one business day.
Engineering Reference: Power, Head Size and Line Speed Matching
Once you move off a handheld wand and onto an inline sealer, the single most common sizing mistake is picking a head that is too small for the cap diameter. A 1.5 kW head that seals a 28 mm PET cap at 60 BPM cleanly will struggle on a 89 mm sauce jar even at 20 BPM, because the coil must deliver enough energy to heat a much larger foil disc in the same 0.5–1 s dwell. We size heads on three numbers together: cap diameter, target bottles per minute (BPM), and product / container temperature. Run any one of them outside the head’s envelope and you trade throughput for seal quality, which on a food or pharma line is not an acceptable trade.
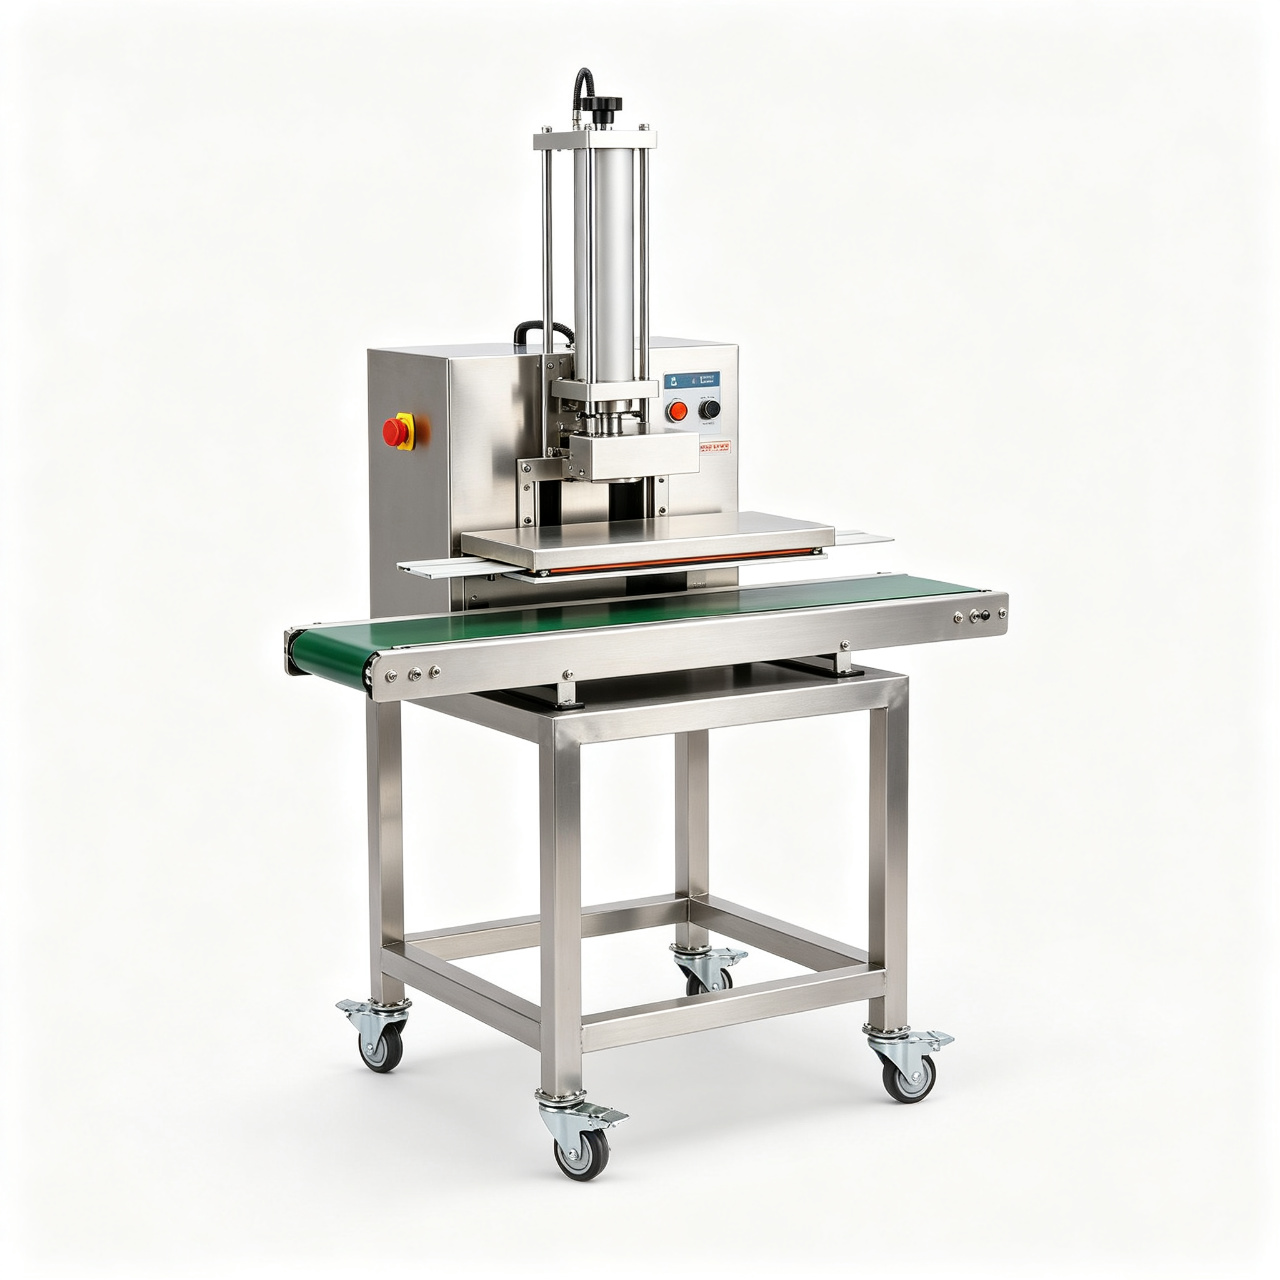
The table below is the starting point we hand to customers during 72-hour FAT runs in our 48,000 m² Qingdao plant. These are not marketing numbers — they reflect what survives a full shift of real product, real bottles, and a 3°C ambient swing. Exact BPM depends on liner thickness, resin, and product temperature, so treat the right-hand column as a ceiling you back off from during seal development, not a spec you push to.
| Head power | Cap / neck diameter | Max line speed (typical) | Where it lands on a filling line |
|---|---|---|---|
| 1.5 kW (air-cooled) | 20–50 mm | up to 40–50 BPM | Pharma syrups, dropper bottles, small cosmetic vials |
| 2.0 kW (air-cooled) | 20–65 mm | up to 60–80 BPM | Food jars, condiments, shampoo, 500 ml beverages |
| 3.0 kW (air-cooled) | 30–89 mm | up to 100–120 BPM | Edible oil, dairy, large supplement bottles |
| 5.0 kW (water-cooled) | 50–120 mm | up to 150 BPM | 1 L sauce jars, peanut butter, 1 L motor oil |
| 8.0 kW (water-cooled) | 89–200 mm | up to 200 BPM+ | Gallon jugs, 5 L buckets, pails, large tubs |
Rule of thumb: size the head for the largest cap on your line, then derate by 20–30% so you are not running the generator at 100% output on every bottle. A head permanently pinned to maximum power is a head that will drift in output as the coil heats up, which shows up as weak bonds by hour four of a shift.
Coil diameter vs cap diameter
The copper coil (sealing head) is formed to your cap. As a starting point, coil inner diameter should sit 3–8 mm larger than the cap diameter — small enough that the field couples tightly to the foil, large enough that the cap top does not physically hit the coil on taller caps. If you run a multi-SKU line with caps ranging 28 mm to 63 mm, plan on two or three swappable heads rather than one compromise coil; a compromise coil seals the middle cap well and the extremes poorly. We document this on the line expansion reference we put together for customers retrofitting a second SKU onto an existing sealer.
Material and Container Compatibility
Induction sealing (or liner sealing, as it is often called on the line) only works because the foil disc is conductive. If the bottle rim cannot be wetted by the heat-seal layer on the back of that foil, no amount of kW will save you. We see more lines delayed by a container swap than by a generator problem. The short compatibility list below is what we walk customers through during seal development.
| Container / liner | Induction seal behavior | What to watch |
|---|---|---|
| PET bottle + standard PE foil liner | Excellent. Lowest power, fastest line. | Thin-wall PET (<0.25 mm) can neck-distort if dwell is long; start at 0.3–0.5 s. |
| HDPE jar + standard PE liner | Good, but needs hotter / longer dwell. | HDPE surface energy is low. Add 15–20% time or move to a corona-treated liner. |
| PP jar + polyolefin-grade liner | Workable with the correct liner grade. | Do not run a standard PE liner on PP — it peels in sheets. Spec a PP-specific seal layer. |
| Glass jar + lacquer-coated foil | Works, but line speed drops 20–40%. | Glass mass draws heat away. Use lacquer-coated foil, not PE, and expect longer dwell. |
| Metal can / metal neck finish | Not suitable for induction sealing. | The metal neck itself heats up, arcing and warping the cap. Use a twist-off / lug closure instead. |
| Foam liner only (no aluminum foil) | Induction cannot work at all. | There is no conductive layer to heat. Swap to a foil-laminate liner before blaming the sealer. |
The two failure modes we get called on most are (a) a customer switching from PET to HDPE without re-running seal development, and (b) a glass jar ordered with a PET liner by mistake. Both show up as a clean peel-off that leaves the rim dry. Both are fixed by changing the liner specification, not by cranking power.
Field Diagnosis: Burn-Through, Flash and Weak Bonds
The earlier defect table covers the five symptoms you see on the line; this section treats the same liner sealing problems from a QA angle. This section goes one level deeper, because in production the difference between burn-through and a weak bond is the difference between a rejected bottle and a leaking one that reaches a customer’s shelf. Seal integrity on a bottled product is a QA conversation, not just an operator one — we teach this during commissioning on every line we ship.
| Defect | What you see on the rim | Root cause | Countermeasure |
|---|---|---|---|
| Burn-through | Foil holed, cap top discolored brown / blistered | Power too high, gap <2 mm, dwell too long, or coil mismatched to cap | Drop power 15–20%, raise gap to 4–6 mm, shorten dwell; verify coil inner diameter |
| Incomplete seal | Peel test shows an un-bonded arc, usually at the back of the neck | Bottle off-center under coil, liner shifted in cap, cap torque too low | Re-guide conveyor, recenter coil, confirm liner sits flat, set cap torque 8–15 in-lb for 28 mm |
| Wrinkled liner | Foil crinkled, not flat to the rim; visible wrinkles under the cap | Bottle wandering, cap applied crooked, liner diameter slightly too large | Install side-guide rails / star wheel, check capper chuck alignment, spec correct liner diameter |
| Flash / squeeze-out | Bead of PE squeezed onto the outer neck; sticky rim | Over-dwell, cap over-torqued, liner too thick | Reduce dwell 0.1–0.2 s, lower cap torque, move to a thinner foil / PE stack |
| Weak bond | Foil peels off in a clean sheet with no PE residue on the rim | Liner grade wrong for resin, cold product chilling the rim, neck contaminated with product | Match liner to bottle resin, pre-warm slow line, install neck cleaner / air knife before capper |
When a line reports mixed results — some bottles seal, some don’t, with no obvious pattern — the cause is almost never the sealer. It is the upstream capper applying inconsistent torque, or the filler leaving a product smear on the neck. Pull ten rejected bottles and look at three things: cap torque variance, neck cleanliness, and bottle height consistency. On a well-tuned line, induction sealer power is the last thing you change, not the first.
Integration on a Filling–Capping Line
Where the sealer sits on the line matters more than engineers expect, and it is the single biggest lever for leakage prevention on a bottled product. The correct position is immediately after the capper and before the labeler or date coder. Put it any earlier and the cap has not been torqued down, so the liner floats above the rim and you get incomplete seals. Put it any later — after the labeler — and a burned-through foil can scorch a plastic label, which means an ugly reject and a wasted label. The sequence is straightforward: fill, cap & torque (the cap sealing step), induction seal, code, label, case.
Three integration details cause the most field callbacks, and they are all cheap to get right the first time:
- Centered conveyor travel. The bottle must pass under the coil on the same centerline every time. Wandering laterally by even 5 mm shows up as a partial seal on one side. Use side-guide rails or a toothed belt between the capper outfeed and the sealer infeed, not a loose roller conveyor.
- Bottle-height sensor. The head should have a no-bottle / wrong-height interlock so power does not fire on a missing cap or an over-tall bottle. This is a 30-minute PLC tie-in and saves a ruined coil.
- Reject synchronization. Tie a vision or torque signal into the sealer’s batch log so a rejected bottle is pulled at the same station regardless of which defect caused it. We cover this in the line integration guide we wrote for multi-station filling lines.
If you are building a new line rather than retrofitting, spec the induction sealer at the same time you spec the liquid filling machines and capping machines — conveyor width, headroom, and star-wheel spacing all interact. The capper in particular needs to deliver consistent torque; we have a capping torque guide that spells out the torque window you should hand to your capper vendor. A line that fills and caps well but seals poorly is usually a capper problem, not a sealer problem. For a budgetary order of magnitude, our filling–capping line cost reference breaks out what the induction station contributes to total line capex.
SunAura has built filling–capping–sealing lines for export in over 100 countries across our 18+ years, every unit FAT-tested for 72 continuous hours in Qingdao under CE and ISO 9001 controls before it ships. The induction station gets the same treatment: we run real bottles, real caps, and real liner material through the sealer on our floor, peel-test the output, and hand the customer the power/time recipe before the crate leaves the loading dock.
More Induction Sealing Questions
What induction sealer power do I need for a 38 mm cap running 100 BPM?
A 3 kW air-cooled head is the typical match. A 2 kW head will seal the cap cleanly but will not hold 100 BPM without drifting toward maximum power, which creates weak bonds late in a shift. Size up to 3 kW and derate to 60–70% output for a stable recipe.
Can I add induction sealing to an existing line without redesigning the conveyor?
Almost always yes. The sealer mounts over a section of existing conveyor; the only conveyor work you usually need is adding side-guide rails so the bottle stays centered under the coil. Head height adjusts to your bottle range, and the unit drops in after the capper. Most retrofits fit inside a weekend.
What is the difference between air-cooled and water-cooled induction heads?
Air-cooled heads (typically up to 3 kW) pass cooling air over the coil and run unattended. Water-cooled heads (5 kW and up) use a closed water loop because they run long enough and hot enough that air cannot dissipate the heat. If your line tops out at 3 kW you do not need a chiller; if you are sealing gallon jars or running 150 BPM, plan for the water loop.
How do you confirm seal integrity in production, not just at FAT?
Pull a sample every 30–60 minutes: peel one bottle (foil must come off in one disc with PE fully wetted to the rim), run a vacuum-decay test on a second bottle, and drop a third from 1.2 m. Log power, time, and gap for the batch. On pharma lines this log is part of the validation record regulators expect; on food lines it is the fastest way to catch a drift before it becomes a leak in the field.