
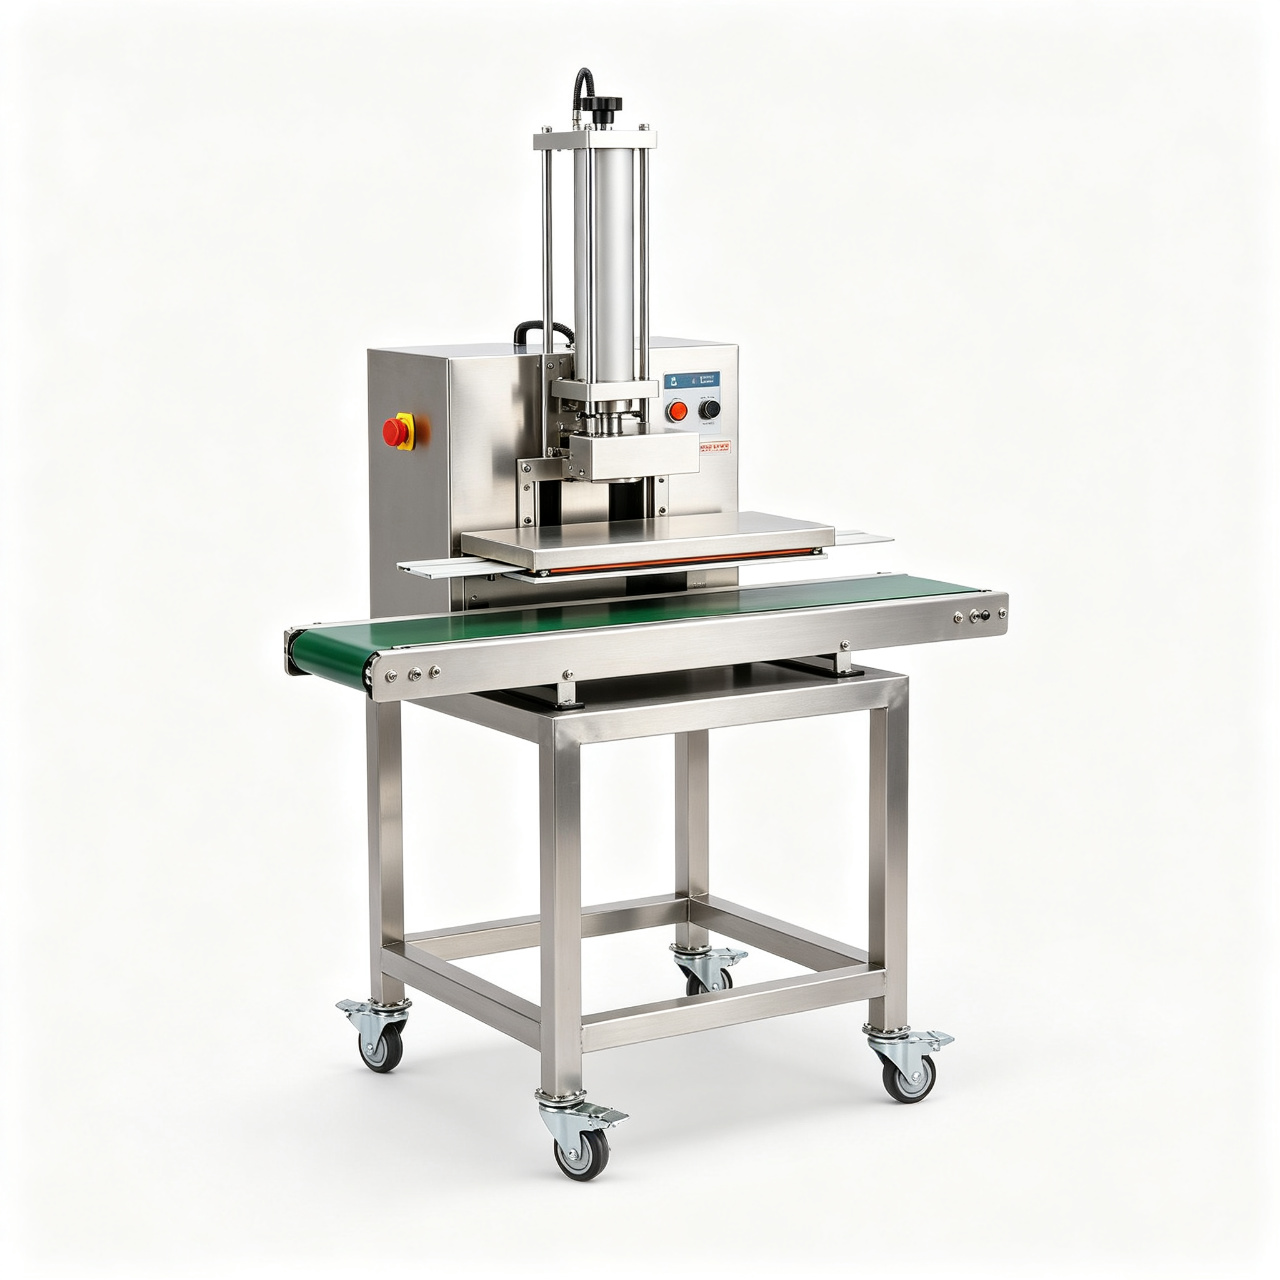
Automatic Induction Sealing Machine for PET Bottles
An induction sealer built for PET bottles on beverage and water lines, matching the smaller coil and shorter dwell that thin-wall PET necks require.
| Output | 50 – 90 containers/min |
|---|---|
| Head | Single sealing head |
| Accuracy | seal integrity test |
| Price band (FOB) | see specification |
| Lead time | see specification |
1. Who this machine is for, and who should not buy it
This machine is bought by producers who need a hermetic seal under a screw cap and want to keep using the same cap they already buy. The foil liner is bonded to the neck by an electromagnetic field, the cap stays on as the mechanical closure, and the result is a container that holds pressure and passes a leak test without any glue or liner insertion on the filling line.
It is the wrong choice when the product needs a sterile barrier rather than a leak-proof one, when the neck is deformed or oval, or when the container is a wide-mouth jar with a foil diameter above 150 mm and a wall thick enough to absorb the field before it reaches the liner. Those cases need conduction sealing or a different closure system.
The realistic buyer profile is a food, chemical, cosmetic or pharmaceutical producer running 30 to 200 containers per minute on a conveyor they already own, with two to six neck sizes across the product range, who wants to add tamper evidence and leak protection without changing caps or the filling machine.
2. How it works
A high-frequency current is driven through a water-cooled coil inside the sealing head, producing an alternating magnetic field. The aluminium foil in the cap liner absorbs the field, eddy currents heat the foil in a fraction of a second, and the polymer coating on the foil melts and fuses to the neck. The cap is not heated, and neither is the product, which is why the method suits heat-sensitive fills.
The cycle is short: the head descends or the container passes under a fixed head, the field is applied for a set time, the foil reaches sealing temperature, the field stops, and the seal cools under the still-tightened cap. Total dwell is typically 0.3 to 1.5 seconds depending on foil thickness, neck diameter and generator power.
What separates a good installation from a marginal one is the match between generator power, coil geometry and neck diameter. An oversized head on a small neck wastes energy and can scorch the liner; an undersized head on a large neck produces a seal that looks closed but fails a pressure test six hours later.
3. Configuration matrix: what changes and what it costs you
The same base frame is sold in several configurations, and the differences matter more than the marketing names suggest. The table below maps each configuration to the buyer profile it actually fits, so you can rule out options before they appear in a quotation.
| Configuration | Heads | Typical output | Container range | Best for | Trade-off |
|---|---|---|---|---|---|
| Hand-fed single head | 1 | 20 – 40 containers/min | 20 – 60 mm neck | Small batch, laboratory, sample runs | Operator dependent, no rejection control |
| Conveyor-mounted fixed head | 1 | 40 – 80 containers/min | 20 – 100 mm neck | Continuous lines with steady pitch | Needs a stable conveyor speed |
| Continuous with height adjustment | 1 | 60 – 120 containers/min | 30 – 150 mm neck | Multi-SKU lines with varying bottle heights | Motorised height change adds cost |
| Water-cooled high-power head | 1 | 60 – 120 containers/min | 60 – 150 mm neck | Wide-mouth jars and thick foil | Requires a chiller or a closed water loop |
The head is the expensive part and the part that must match your neck range. Buyers who plan three neck sizes usually need either two heads or a head with an adjustable coil; buying one head sized for the largest neck and running it on small necks is the most common cause of scorched liners.
4. Technical specifications
Figures below are the standard build. Every value can be changed, but each change moves price, lead time and the commissioning effort, so read the notes column before asking for a variant.
| Parameter | Standard | Optional / range | Why it matters |
|---|---|---|---|
| Sealing head | Single, water-cooled | Two heads for dual-lane | Head geometry must match neck range |
| Neck range | 20 – 38 mm | Custom coil per neck size | Outside the range the seal fails silently |
| Output | see specification | Up to 120 containers/min | Quoted on a matched conveyor |
| Generator power | 1.5 – 4 kW | Up to 6 kW for wide-mouth | Power follows foil area, not bottle size |
| Frequency | 20 – 40 kHz | Fixed by generator model | Higher frequency suits thin foil |
| Foil type | Aluminium 20 – 40 µm | 38 µm for aggressive products | Thinner foil seals faster and weaker |
| Cooling | Air cooled | Water cooled for continuous duty | Air cooling limits duty cycle |
| Conveyor | Stainless slat or belt | Speed-synchronised to line | Pitch stability decides seal consistency |
| Height adjustment | Manual | Motorised with recipe memory | Multi-SKU lines need motorised |
| Rejection | Optional | Cap presence + seal check | Without it, failures reach the pallet |
| Power supply | 380 V three-phase | 220 V single phase for small units | Confirm before order |
| Guarding | Interlocked hood | CE-compliant safety circuit | Field exposure is the risk to guard |
5. Throughput and capacity planning
Output is set by conveyor speed and head dwell, not by the generator. At a 1.2 second dwell and a 150 mm pitch, one head tops out near 50 containers per minute; the same head on a 60 mm pitch reaches about 120. Buyers who quote a speed without quoting pitch are comparing incomparable numbers.
Plan on 70 to 80 % of the theoretical figure. The losses come from cap-present faults, missing foil liners, height adjustment between SKUs and the stops that happen whenever the upstream filler pauses.
If your line runs multiple SKUs with different bottle heights, add the motorised height adjustment at order. Manual adjustment is fine for a single format and becomes a bottleneck the moment you run three.
| Shift pattern | Gross output | OEE at 65% | Annual bottles (300 days) |
|---|---|---|---|
| 1 × 8 h | 120 bph | 78 bph | 187,200 |
| 2 × 8 h | 120 bph | 78 bph | 374,400 |
| 3 × 8 h | 120 bph | 78 bph | 561,600 |
Size the machine on the middle of the range, not the top. A unit sold at 120 bottles per hour that runs at 120 for six hours a day is being asked to live at its mechanical limit; the same unit at 90 bottles per hour has headroom for viscosity drift, cap changes and the occasional slow batch.
6. Product and container fit
Fit depends on neck geometry and foil, not on product. A round neck with a flat sealing surface seals reliably; an oval or dented neck does not, because the field concentrates at the closest point and the foil fails to bond around the circumference.
Products with a high water content and a low headspace are easier; products with oil on the neck rim, or powder contamination on the sealing surface, need a clean neck or the bond fails regardless of machine quality.
| Product type | Viscosity band | Fit | What to watch |
|---|---|---|---|
| PET bottles, water and juice | 20 – 38 mm | Excellent | Neck must be dry and undented |
| HDPE bottles, chemicals | 28 – 63 mm | Excellent | Check foil compatibility with the product |
| Glass jars, food | 38 – 100 mm | Good | Thicker wall needs more power |
| Wide-mouth jars | 100 – 150 mm | Conditional | Water-cooled head and higher power required |
| Tubes and small vials | 13 – 20 mm | Conditional | Small coil, low power, precise dwell |
| Oval or deformed necks | any | Not suitable | Field concentration causes partial seals |
7. Selection decision framework
Use these rules in order. Each one is a hard filter, not a preference, and each is written so that two buyers with different constraints reach different answers rather than the same recommendation.
Rule 1: Neck diameter first
Below 20 mm you need a small dedicated coil and a short dwell. Above 100 mm you need water cooling and 4 kW or more. In between, a standard head covers the range.
Rule 2: Foil specification second
A 20 µm foil seals fast and is right for water-based products. A 38 µm foil is right for aggressive chemicals and for containers that will be shipped under pressure, but it needs more power and a longer dwell.
Rule 3: Conveyor stability third
A conveyor that surges produces seals that vary from strong to weak on the same batch. If your conveyor is driven by the filler through a mechanical link, expect variation; a separate drive with a speed encoder fixes it.
Rule 4: Rejection fourth
Without cap-present detection and a seal check, failures are found by the customer. Add the rejection station at order; retrofitting it later costs more than the station itself because the line has to be re-plumbed.
Rule 5: Cooling fifth
Air cooling is adequate up to about 60 containers per minute in a temperate plant. Above that, or in a hot room, water cooling is the difference between a stable seal and a head that derates itself.
Rule 6: Compliance sixth
CE marking requires an interlocked hood and a documented field-exposure assessment. Buyers in regulated markets should ask for the assessment, not just the certificate.
8. Alternatives compared head to head
The alternatives are not other induction machines but other ways to close the same container. Each has a different cost, a different maintenance profile and a different failure mode, and the choice usually comes down to how much seal integrity the product actually needs.
| Criterion | Automatic Induction Sealing Machine for PET Bottles | Induction foil sealing | Conduction sealing | Glue / liner-free closures |
|---|---|---|---|---|
| Seal type | Hermetic foil bond | Heat-sealed liner | Mechanical only | see specification |
| Cycle time | 0.3 – 1.5 s | 2 – 5 s | n/a | see specification |
| Heat into product | None | Local, can affect fill | None | see specification |
| Neck tolerance | Needs round, flat neck | Needs flat land | More forgiving | see specification |
| Consumable | Foil liner in cap | Liner or film | None | see specification |
| Maintenance | Coil and cooling circuit | Heated die wear | Cap torque only | see specification |
| Best fit | Leak-proof food, chemical | Thick-wall jars, low volume | Dry products, short life | see specification |
Conduction sealing is cheaper per unit and slower per container, and it puts heat into the neck, which matters for heat-sensitive fills. Glue-free closures are cheapest and offer no leak protection at all, which is acceptable for powders and unacceptable for liquids.
9. Line integration
The sealing head is normally mounted on the conveyor between the capper and the labeller. Upstream, the cap must be fully tightened: a loose cap lets the foil lift during sealing and produces a weak bond that passes a visual check and fails a pressure test.
Downstream, allow 300 to 500 mm of cooling conveyor before the labeller or the case packer so the seal sets under compression. Lines that label immediately after sealing show a higher failure rate, and the cause is usually attributed to the sealer when it is actually the absence of cooling distance.
Signals worth agreeing: container-present, head-ready, fault relay, and a reject output if a rejection station is fitted. If the sealer is fed by a filler through an accumulation table, confirm the accumulation does not let containers sit under the head, which scorches liners.
10. Hygiene, materials and compliance
The head and coil are water-cooled and sealed; the housing is stainless on washdown builds. Because the field does not touch the product, hygiene requirements are mainly about the surfaces that contact the container and about cooling-water integrity.
Documentation for a food or pharmaceutical audit typically includes material certificates for the contact surfaces, a field-exposure assessment, and a seal-integrity test protocol with the acceptance criteria you will apply. Ask for the protocol before the machine ships, because the criteria decide whether the machine passes.
If the machine runs in a wet room, specify IP65 electrics and a stainless frame at order. Retrofitting a cooling circuit and sealed electrics into a running line means a shutdown and a new cabinet.
11. Installation and commissioning
| Stage | Duration | Who does it | Deliverable |
|---|
Commissioning is three to five days for a conveyor-mounted sealer. The two items that most often delay it are conveyor pitch alignment and the availability of production containers with the correct caps and liners, so book both before the machine arrives.
12. Maintenance, spares and uptime
The coil and the cooling circuit are the two items that need attention. A coil that has been run hot loses efficiency and produces weak seals before it fails outright, so a weekly seal test is a better indicator than a visual inspection.
Keep a spare coil for your most common neck size and a spare set of cooling hoses. Both are inexpensive relative to the downtime they prevent, and a coil failure without a spare typically means two to three weeks of air freight.
| Wear part | Interval | Cost band | Downtime if ignored |
|---|---|---|---|
| Sealing coil | 12 – 24 months | US$ 180 – 600 | Weak or partial seals |
| Cooling hoses | 12 months | US$ 40 – 90 | Head derates and stops |
| Generator capacitor | 24 – 36 months | US$ 60 – 150 | No field, no seal |
| Conveyor belt | 12 – 24 months | US$ 80 – 220 | Pitch drift, inconsistent dwell |
13. Cost structure and total cost of ownership
The purchase price is a smaller share of the five-year cost than for a filling machine, because the consumable foil liner and the seal-testing labour add up. Buyers who compare machines on price alone often miss that a badly matched head consumes more power and more liner failures.
A useful check is cost per thousand containers sealed, including the foil liner, the power and the rejection rate. A cheaper machine that rejects 2 % more containers usually costs more than the difference in price within the first year.
| Cost line | Typical band | Notes |
|---|---|---|
| Machine, FOB | US$ 3,500 – 18,000 | Depends on head size and cooling |
| Foil liners | US$ 0.004 – 0.02 per container | Consumable, per cap |
| Power | US$ 0.15 – 0.40 per 1,000 | Generator duty cycle matters |
| Cooling water | US$ 0.05 – 0.15 per 1,000 | Closed loop reduces this |
| Spares, year 1 | US$ 300 – 800 | Coil, hoses, belt |
| Seal testing labour | 15 min per shift | Destructive sample per head per shift |
14. RFQ checklist
A quotation is only as precise as the inputs behind it. Buyers who send these fourteen data points in the first email typically receive a firm price and a layout drawing on the first reply; buyers who send "a filling machine, about 5,000 an hour" spend three rounds establishing what that means.
15. Quality assurance and FAT documentation
Factory acceptance for a sealer is a seal-integrity test, not a speed test. We seal thirty containers per neck size, cut them open to inspect the bond, and pressure-test a sample. The report records the dwell, the power setting and the foil specification used.
Ask for the test report with the settings, because the seal depends on the combination. A machine that passes with 38 µm foil at 4 kW may fail with 20 µm foil at 2 kW on the same neck, and a report without the settings cannot be reproduced.
16. Frequently asked questions
Does the cap have to be a specific type?
No, but the cap must contain an aluminium foil liner with a polymer coating compatible with your product. Standard screw caps with induction liners work; caps without a foil liner cannot be sealed by this method.
Can it seal through a plastic cap?
Yes. The field passes through the plastic cap and heats only the aluminium foil, which is why the cap is not damaged and the product is not heated.
What dwell time should we use?
Start at 0.8 seconds for a 30 mm neck with 20 µm foil and adjust until the bond is complete but the liner is not scorched. The correct setting is found by cutting open samples, not by looking at the cap.
Why do some seals fail a pressure test?
Usually three causes: a damp or contaminated neck, a loose cap that lets the foil lift, or a head that is undersized for the neck diameter. Each has a different fix, and the test report should identify which one applies.
Is rejection equipment necessary?
Without it, failures are found downstream, often by the customer. Cap-present detection is cheap and catches the most common failure; a seal-integrity check catches the rest. Both are worth fitting at order.
How often should the coil be replaced?
Typically every 12 to 24 months depending on duty cycle. A weekly seal test on a sample tells you when the coil is losing efficiency before it fails completely.
17. Footprint, utilities and infrastructure
Site planning fails more often on ceiling height and drain position than on floor area, so check these three numbers before the layout is drawn: the height needed for nozzle lift plus the tallest container, the distance from the machine to the nearest drain, and the free capacity on your compressed-air ring main at shift start, when every other machine is also drawing air.
| Item | Requirement | Note |
|---|---|---|
| Floor area | 2.4 x 1.3 m for the machine, plus 1.2 m service access on each side | Access is for the mechanic, not for the operator |
| Ceiling height | 1.9 m minimum above the frame | Nozzle lift plus container height |
| Power | 3 kW, 380 V three-phase, 50 or 60 Hz | Separate circuit with earth, not shared with welders |
| Compressed air | 0.6 MPa, 0.4 m3/min free capacity | Dry air; moisture causes valve sticking |
| Drain | Within 1.5 m of the machine | For washdown and for the drip tray outlet |
| Noise | Under 75 dB(A) at 1 m | Most of it comes from the vacuum pump or blower, not the filler |
A common mistake is to install the machine against a wall to save floor space. The service access on the left side is where the mechanic reaches the drive and the valve manifold; blocking it turns a fifteen-minute job into a two-hour dismantling job, and in practice it also means the machine is never serviced properly.
18. Application scenarios by industry
The same machine is bought for very different reasons, and the configuration that suits one industry is often wrong for another. These four patterns cover most of the enquiries we receive, and each one points to a different set of options.
Food and beverage producers usually need washdown-capable surfaces, food-contact declarations and a changeover fast enough to run three products in a shift. Their decision is driven by the retailer audit, and the machine is specified with stainless frame, IP65 electrics and removable nozzles. Their biggest hidden cost is not the machine but the changeover labour they did not plan for.
Cosmetic and personal-care producers fill smaller volumes at lower output, and their constraint is appearance: no drips on the bottle shoulder, no product in the thread, consistent fill line across a batch. They need a back-suction or suck-back nozzle and a slower final approach more than they need speed, and they usually regret buying a machine sized for output rather than for cleanliness.
Pharmaceutical and diagnostic producers buy documentation as much as hardware. The filling head is secondary to the material traceability, the validation package and the ability to prove that cleaning was effective. Their machine is 316L, their seals are PTFE, and their acceptance test is a written protocol rather than a visual check.
Chemical and household producers fill corrosive or volatile liquids where the wetted material and the seal elastomer decide the machine life. They need Viton or PTFE seals, a stainless frame, and often an extraction hood over the filling zone. Accuracy is less critical than containment, and the machine should be specified accordingly.
19. Supplier evaluation: seven questions with answers you should accept
Buying a filling machine is a comparison between suppliers as much as between machines, and the difference shows up in the second year rather than the first. These seven questions are the ones that separate a supplier who builds machines from one who resells them, and each has an answer you can check against a document.
1. Can you show the calibration record for every head?
A serious supplier weighs thirty bottles per head and reports mean and standard deviation per head, not a single number for the machine. If a head is 2 % off while the average looks fine, the record exposes it and the machine should not ship.
2. What is the spare-part lead time for wear items?
Nozzle seals and valve seats should be shippable in under a week from stock. If the answer is "we order from the OEM", your machine stops for two weeks the first time a seal fails, and seals always fail.
3. Who signs the acceptance test, and against what criteria?
The criteria should be written before the order, in numbers: output over four hours, volume tolerance, drip count, reject rate. A supplier who will not commit to numbers is telling you the numbers are not stable.
4. What is the changeover procedure, and who can perform it?
An operator should be able to change format in under ten minutes with a recipe call and one tool. If the answer involves a mechanic and a spanner, add the labour cost to your five-year total before you compare prices.
5. Which parts are bought in, and from where?
Servo drives, PLCs, pneumatic valves and load cells are branded components, and their availability in your region decides whether a breakdown is a two-day or a two-month event. Ask for the brand list and check local distribution before you sign.
6. What does commissioning include, and what costs extra?
Installation, calibration, training and a production trial should be itemised. The expensive surprises are usually crane hire, extra engineers beyond the agreed days, and re-commissioning after your utilities turn out to be out of specification.
7. Can we speak to a customer running the same product?
A supplier with a real installed base can name two or three references on request. Vague answers here are the single strongest signal to slow down.
20. The first 90 days after arrival
The first three months decide whether the machine settles into a rhythm or becomes a source of daily firefighting. Most of what goes wrong in this window is procedural rather than mechanical, and it is fixable if it is watched.
Days 1 to 10: install, level and align to the conveyor, verify rotation direction and air pressure, then run empty containers through every station by hand before powering the filling circuit. Record the as-built settings in the manual rather than on a note taped to the frame.
Days 11 to 30: calibrate each head on your own product at your own filling temperature, then run a full shift at 70 % of rated output and log volume every hour. The drift pattern in this shift predicts the maintenance interval better than any manual.
Days 31 to 60: train a second operator and one mechanic, not just the person who will run the day shift. Single-person knowledge is the most common cause of a line that cannot run at weekends or during holidays.
Days 61 to 90: review the reject log, count the stops and their causes, and set the first preventive-maintenance dates from the real failure pattern rather than the generic intervals in the manual. Order the first spare kit before the end of this window, because the first seal failure usually arrives around month four.
21. Specification mistakes that cost buyers money later
Nearly every unhappy installation traces back to a decision made in the quotation stage, when a number was accepted without being checked. These six mistakes appear often enough to be predictable, and each is cheap to avoid at order and expensive to correct after arrival.
Accepting output quoted without container details
A speed quoted in bottles per hour means nothing until it is tied to a fill volume, a neck diameter and a product viscosity. Ask for the test conditions in writing: 500 ml, 28 mm neck, water at 20 °C is a very different machine from 1 L, 18 mm neck, syrup at 12 °C.
Buying the maximum head count the budget allows
More heads raise output, but they also raise air consumption, spill risk, calibration work and the cost of every future seal replacement. A machine with eight heads running six days a week at 80 % utilisation beats a twelve-head machine running three days at 45 %.
Forgetting the conveyor pitch
The filling machine, the capper and the labeller must share a container pitch and a conveyor height. When they do not, the integrator builds a transfer plate and a pitch change, and the buyer pays for it in commissioning time and in jams that never quite disappear.
Under-specifying the electricals
IP65 electrics, a separate earth and a dedicated circuit cost a few hundred dollars at order. Retrofitting them into a running line costs a shutdown, a new cabinet and an electrician, and until it is done the machine is a washdown hazard.
Buying seals by price
A seal that costs two dollars less and lasts half as long doubles your maintenance labour and adds a failure mode in the middle of a production run. Specify the elastomer by product compatibility, not by unit cost.
Treating training as a formality
Two days of training with written SOPs is the cheapest reliability investment available. Buyers who skip it usually spend the same money later on a service visit to fix problems the manual already described.
22. Comparing quotations line by line
Three quotations for the same nominal machine can differ by 40 % and still describe the same hardware, because what sits inside the price is different. The line-by-line comparison below is the one we recommend to buyers, and it is also the format our own proposals follow so that the differences are visible rather than buried in a total.
What should be inside the base price
The base price should include the machine as specified, one set of tooling for the agreed format, the control system with its recipe memory, guards and interlocks, an English manual, a tool kit and a spare seal set. If any of those appear as separate lines in a competing quotation, the totals are not comparable and the cheaper number is usually the one with more excluded.
What should be quoted separately, and why
Freight, insurance, duties, installation, training beyond the included days, custom tooling and optional inspection equipment should be separate. That is not a trick; it lets you see the cost of each decision. The trick is the opposite: a single lump sum that hides a two-week commissioning visit inside a number you cannot audit.
Warranty terms
Compare the duration, what is covered, who pays the freight on a warranty part, and what voids the warranty. Twelve months on parts with buyer-paid freight is very different from twelve months including freight and labour. Ask for the wording, not the summary.
Payment schedule and risk
Thirty per cent deposit and seventy per cent against documents is the common structure for export. A supplier asking for the full amount before dispatch is asking you to carry all the risk; a supplier accepting ten per cent deposit is carrying it themselves. The schedule tells you something about who expects to have problems.
Lead time and its components
Ask for the split between engineering, procurement, assembly, testing and packing. A lead time of forty days that is thirty days of waiting for a servo drive is a different risk from forty days of assembly. When a date slips, the split tells you whether to push the supplier or the component.
23. Questions procurement teams ask us most often
Can you supply the same machine on 415 V, 60 Hz?
Yes. Voltage, phase and frequency are specified at order because they change the motors, the drives and the transformer sizing. Changing them after the machine is built means replacing components, and it is one of the few specifications that cannot be adjusted on site.
What is the actual delivery time to our port?
Production lead time is 25 to 45 days, sea freight to most destinations is 18 to 35 days, and port-to-door adds three to ten days depending on customs. The total is what your planning needs, and it is usually 8 to 12 weeks from order to a machine running in your plant.
Do you provide a local installation service?
We send engineers from the factory for installation and commissioning, and for repeat buyers we can arrange a local partner for routine service. Installation by the factory team is the option we recommend for a first machine, because it transfers the process knowledge as well as the hardware.
What happens if a part fails in the first year?
Warranty parts ship by air within three working days of a confirmed diagnosis, and we ask for photographs and the fault code so the diagnosis is right the first time. For critical wear items we recommend holding a local kit, which costs a few hundred dollars and removes the air-freight delay entirely.
Can the machine be audited before we release the balance?
Yes. The factory acceptance test is the natural point: you or your third-party inspector attend, watch the run, review the calibration data and the material certificates, and the balance is released against a signed report. Buyers who skip this step sometimes discover a specification mismatch only after the container arrives.
24. Service levels, response times and what we commit to in writing
Service is the part of a machine purchase that buyers cannot inspect before they pay, which is exactly why it deserves a place in the comparison spreadsheet. What follows is what we put in the contract rather than what we say in a sales meeting, and we recommend asking every competing supplier the same four questions.
Response time
First technical response within one working day of a written query with photographs and the fault code. Remote diagnosis within two days. Where a site visit is needed, an engineer is dispatched within five working days, or sooner if the line is stopped.
Spare parts
Wear items from stock, shipped within three working days by air. Non-stock parts are quoted with a lead time in writing. The recommended spare kit is listed in the manual with part numbers, so you can reorder from any distributor rather than only from us.
Warranty
Twelve months on parts and labour for defects in manufacture, twenty-four months on the frame. Consumables and wear items are excluded, which is normal, but the exclusion list is written down rather than implied. Warranty freight is covered by us for the first shipment of a replacement part.
Training and knowledge transfer
Two days of on-site training are included with commissioning: one day for operators covering start-up, changeover, cleaning and the first line of fault finding, and one day for the mechanic covering adjustment, wear inspection and the spare-parts replacement procedure. Both days end with a written SOP that your team keeps.
What we do not promise
We do not promise a response time measured in hours, because a promise that cannot be kept is worse than a realistic one. We do not promise that a machine will run at its maximum output indefinitely; we promise the tested output on the format and product used at acceptance, and we document the conditions. Buyers who want a guarantee on through-life output should buy a service contract, and we quote those separately so the cost is visible.
Send your container and product details
Send the neck diameter, cap type, foil specification, container material and target output. We will confirm the head size, the power setting and the dwell time, and send a priced proposal with a seal-test protocol.