
Low-Level Case Palletizer
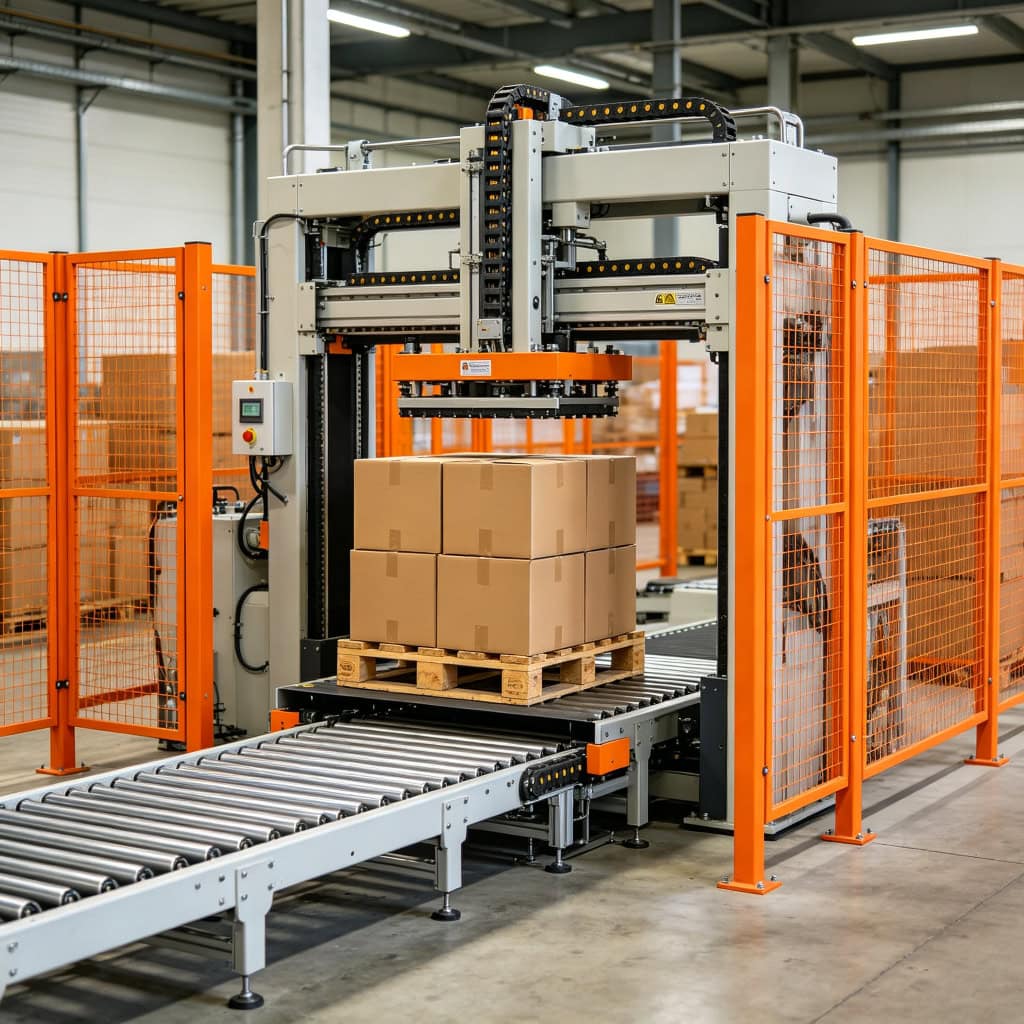
The SunAura SNA-LLP1200 low-level case palletizer brings automated palletizing to facilities where a high-infeed machine simply won’t fit. Cases enter at floor level (800 mm), the layer forms inside a low-profile frame, and the stack reaches 1600 mm without needing a mezzanine or elevated conveyor. Up to 1200 cases/hour in a 4×3 m footprint — the practical choice for medium-speed food, consumer goods, and pharma lines.

Product Description
The SunAura SNA-LLP1200 is a low-level (floor-infeed) automatic case palletizer designed for production facilities with limited ceiling height, existing floor-level conveyor lines, or operators who need easy access to the machine. Cases enter on a conveyor at 800 mm — roughly waist height — travel through a compact layer-forming section, and are stacked onto pallets inside a fully guarded frame. No elevated infeed, no mezzanine, no pit required. The entire machine fits in a 4×3 m footprint and runs on standard 380V 3-phase power.
Unlike high-level palletizers that form layers above the discharge, the SNA-LLP1200 builds layers on a shuttle table and lowers each completed layer onto the pallet below. This keeps the overall machine height under 3.5 m — compatible with standard warehouse and production buildings. Capacity runs up to 1200 cases/hour for cases weighing 3–20 kg. The touchscreen HMI stores up to 20 layer recipes, and the safety guarding package includes interlocked access doors, light curtains at the infeed, and emergency stops at every corner.
This is the model most often chosen by medium-sized food processors, contract packers, and regional distribution centers that want the reliability of automatic palletizing without the civil works and elevated conveyor costs of a high-level system. Every unit is factory-load-tested with customer-supplied cases before shipment, and our engineers provide remote commissioning support via video call after installation.
Technical Specifications
| Model | SNA-LLP1200 Low-Level Case Palletizer |
|---|---|
| Capacity | Up to 1200 cases / hour |
| Case Weight Range | 3 – 20 kg per case |
| Infeed Conveyor Height | Floor-level, 800 mm standard (customizable) |
| Max Stack Height | 1600 mm (on pallet, including pallet) |
| Pallet Size | 1200 × 1000 mm (Eur standard) |
| Machine Footprint | Approx. 4 × 3 m (L × W) |
| Power Supply | 380 V, 3-phase, 50 / 60 Hz (factory-set to order) |
| Control | PLC + color touchscreen HMI, up to 20 recipes |
| Safety Guarding | Interlocked doors, light curtains, emergency stops, CE-compliant |
| Layer Forming | Automatic shuttle-table layer, programmable patterns |
| Certification | CE Certified, ISO 9001 factory |
Key Features & Benefits
- Floor-level infeed, no mezzanine needed: Cases enter at 800 mm from the floor — no elevated conveyor, no platform, no civil works. Drop it onto an existing floor-level line and go.
- Compact 4×3 m footprint: The low-profile frame uses space efficiently, fitting into production rooms that cannot accommodate a high-level palletizer’s vertical reach.
- Operator-friendly access: Service panels and the layer-forming station are at standing height. Clearing a jam or adjusting guides does not require climbing a ladder.
- Up to 1200 cases/hour: Rated for medium-speed lines — fast enough to keep up with most food, beverage, and consumer goods case packers without overspecifying.
- Recipe-driven changeover: Store up to 20 pallet patterns on the HMI. Switch between SKUs in seconds; no mechanical guide adjustment needed for standard case sizes.
- Full safety guarding included: Interlocked access doors, light curtains at infeed and discharge, and four-corner e-stops — CE-compliant and ready for plant safety audits.
- Handles 3–20 kg cases: Covers the full range from light cosmetic cartons to heavy food and beverage cases without mechanical modification.
- Remote commissioning support: Our engineers walk your installation team through setup and first-run via video call — no overseas travel delay before production starts.
Application Industries
Food & Beverage
Packaged foods, snacks, bottled drinks, and canned goods in corrugated cases — reliable stacking for regional distribution and wholesale.
Consumer Goods
Household cleaners, detergents, paper products, and personal care items — cases of varied dimensions handled via recipe changeover.
Pharmaceuticals
Medicine cartons, medical supplies, and OTC products in shipping cases — clean-room-compatible construction with smooth, easy-wipe surfaces.
Small Manufacturing
Regional producers with medium-speed lines that need automatic palletizing without the cost and footprint of a full high-level system.
Contract Packing
Co-packers and 3PL operations handling multiple brands and SKUs — recipe-driven changeover adapts to each customer’s packaging.
Cosmetics & Personal Care
Makeup, skincare, and fragrance cases — gentle handling and clean construction for brand-sensitive products.
Load compatibility: Corrugated cases, trays, and shrink-wrapped bundles weighing 3–20 kg per unit on 1200×1000 mm pallets. For bags (cement, flour, feed), see our Automatic Bag Palletizer. For very light cartons under 2 kg, see our Compact Carton Palletizer.
How Low-Level Case Palletizing Works
Low-level palletizing uses a shuttle-table layer former that builds layers at operator height and lowers them onto the pallet below. The SNA-LLP1200 cycle runs automatically as cases arrive on the floor-level infeed:
- Cases enter at floor level. Upstream equipment discharges cases onto the 800 mm infeed conveyor — the same height as most existing case packaging lines.
- Singulated and oriented. Cases are spaced to a controlled pitch and oriented according to the selected recipe. Sensors confirm position before each push.
- Layer builds on the shuttle table. A push bar places cases side by side on the shuttle table. Side squaring guides keep the layer tight and square as it builds row by row.
- Shuttle table transfers layer to pallet. When the layer is complete, the shuttle table slides over the pallet and lowers, depositing the full layer onto the stack below.
- Repeat to stack height. The shuttle returns, builds the next layer, and lowers. The cycle repeats until the 1600 mm stack height is reached, then the full pallet exits and an empty pallet loads.
Is This the Right Palletizer for You?
The SNA-LLP1200 is the right fit if your operation matches all four of the following. If you fall outside any of them, our team can recommend a different SunAura model:
- Throughput between 300 and 1200 cases/hour: This machine covers medium-speed lines. If you need 1500+ cases/hour, step up to our High-Level Layer Palletizer. If you run under 300 cases/hour, a Compact Carton Palletizer may be more economical.
- Ceiling height under 4.5 meters: The low-level design keeps machine height under 3.5 m. If your building has high ceilings and you want maximum throughput, the high-level model is faster.
- Cases weigh 3–20 kg: Within this range, the layer former and shuttle table handle the load comfortably. Heavier loads (up to 50 kg) need our bag palletizer or heavy-duty robotic model.
- Floor-level infeed available: Your upstream conveyor can feed cases at 800 mm height. If your line already has an elevated infeed at 1800 mm, the high-level model may integrate more cleanly.
Troubleshooting Guide — Common Issues & Solutions
Low-level palletizers are generally less prone to vertical-mechanism issues than high-level designs, but floor-level infeed and compact frames introduce their own common problems. Below are the most frequent issues we diagnose remotely. Always lock out energy sources before reaching into the machine.
| Problem | Possible Causes | Solutions |
|---|---|---|
| Cases enter crooked on the infeed conveyor | Side guides misaligned; upstream case packer off-center; conveyor belt tracking off. |
|
| Layer misalignment on shuttle table | Squaring guides worn; push bar pressure uneven; shuttle table not level. |
|
| Stack leans or collapses before reaching height | Layer pattern not interlocking; cases overhanging pallet; pallet warped or uneven. |
|
| Shuttle table does not slide smoothly | Linear guide rails dirty; chain or belt tension off; lubrication dry. |
|
| Light curtain triggers nuisance stops | Light curtain misaligned; dust on lens; forklift passing through discharge zone; reflection off shiny case film. |
|
| Machine stops with “pallet not detected” alarm | Empty pallet not placed correctly; pallet magazine low; pallet presence sensor dirty or misaligned. |
|
If the issue persists after trying these steps, email photos and a short 10-second video of the problem to [email protected] — our engineers usually diagnose the root cause within one business day.
Frequently Asked Questions
What ceiling height do I need for this low-level palletizer?
The SNA-LLP1200 stands under 3.5 m tall including the safety guards. Plan for 3.8–4.0 m of clear ceiling height to leave room for maintenance access above the machine. This is significantly lower than a high-level palletizer, which typically needs 4.5–5.5 m.
Can it integrate with my existing floor-level conveyor?
Yes. The standard infeed height is 800 mm, which matches most existing case conveyor lines. If your existing conveyor is at a different height, we can customize the infeed to match. Just send us your current conveyor height during quotation.
How many cases per hour in real production?
Rated capacity is up to 1200 cases/hour. Actual output depends on case dimensions and layer pattern — a typical 400×300 mm case on a 1200×1000 mm pallet runs 800–1000 cases/hour in production. We simulate your actual case dimensions before you order.
Does it come with safety guarding, or is that extra?
Safety guarding is included — interlocked access doors, light curtains at infeed and discharge, and four-corner emergency stops are standard on every SNA-LLP1200. The guarding package meets CE machinery safety requirements.
How do operators change over between different case sizes?
Layer patterns are stored as recipes on the HMI. Select the new product recipe and the machine adjusts the push pattern automatically. If the new case size is outside the current guide setting, a 5–10 minute mechanical guide adjustment is needed. Most co-packers keep 10–15 recipes loaded.
What is the lead time and shipping?
Standard models ship in 25–35 days from Qingdao, China. The machine disassembles into sections for container loading. Our engineers provide remote video support during installation and first run. Spare parts are dispatched worldwide within 48 hours via DHL/FedEx.
Why Buy From SunAura Machinery
48,000㎡ Own Factory
In-house manufacturing in Qingdao, China — no middlemen, no trader markup.
CE Certified
All machines meet European safety standards with full documentation.
ISO 9001:2015
Quality management system certified across the entire production process.
SGS Audited Factory
Third-party audited manufacturing facility with 20+ national patents.
12-Month Warranty
Full warranty covering parts and labor from the date of shipment.
Lifetime Support
Technical guidance via email, WhatsApp, and remote video for the machine’s life.
Spare Parts in 48h
Genuine parts shipped worldwide via DHL/FedEx within 48 hours.
100+ Countries Served
Trusted by packaging lines across food, beverage, pharma, and chemicals.
Get a Factory-Direct Quote in 24 Hours
Tell us your case dimensions, pallet size, and expected output — our engineers reply with a model recommendation, FOB price, and lead time within one business day. Every machine is built in our 48,000㎡ Qingdao factory, CE & ISO 9001 certified.
Email [email protected]Related Palletizers
Browse the full range on the palletizers landing page. Also explore our automatic bag palletizers and gantry palletizing systems to build a complete end-of-line solution.