
Heavy-Duty Four-Axis Robotic Palletizer (180kg Payload)
The SunAura heavy-duty four-axis robotic palletizer (SNA-RP180) is built for the toughest end-of-line duty: 25–50kg cement, fertilizer and chemical bags, stacked to tall pallets in dusty, abrasive environments. A 180kg payload, 2600mm reach, reinforced wrist and IP65 protection deliver up to 12 cycles per minute with repeatability of ±0.8mm. Heavy-duty gripper EOAT, 380V 3-phase, CE-certified and factory-direct.

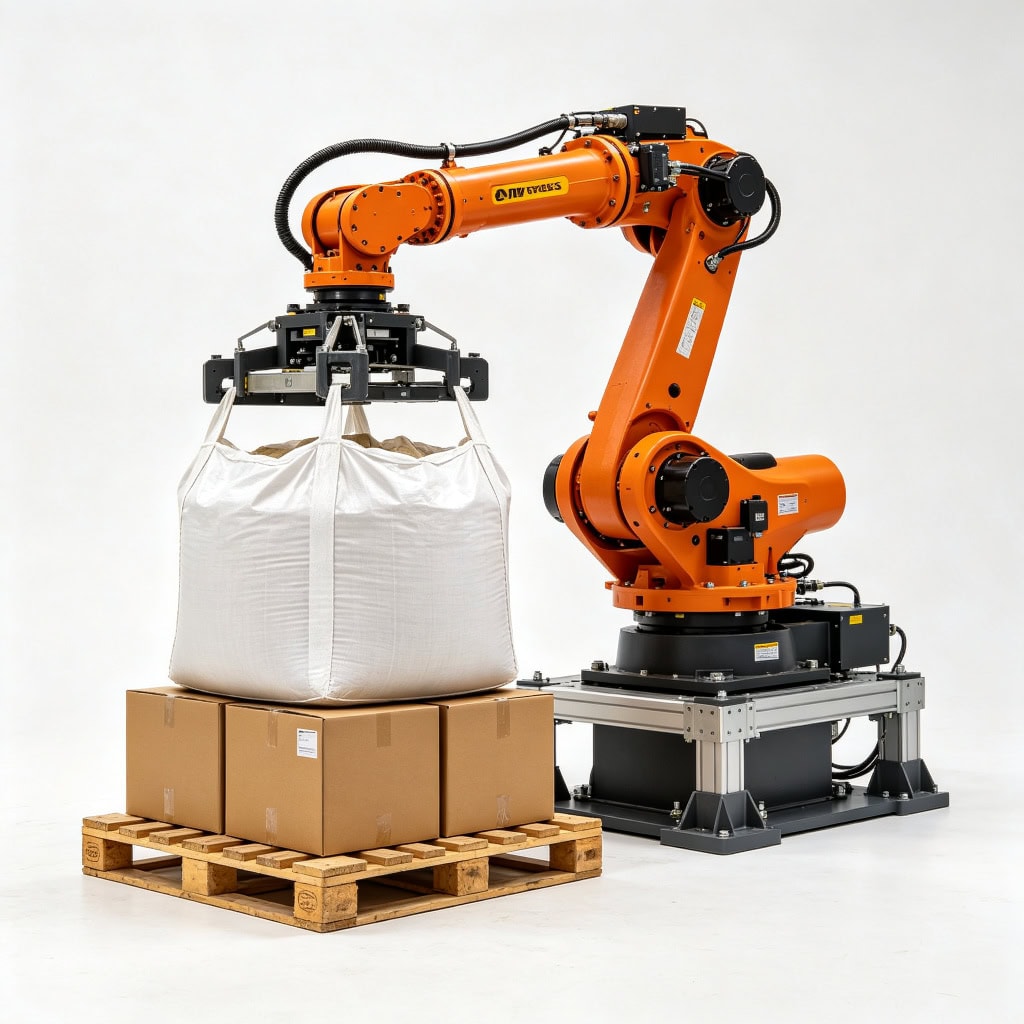
Product Description
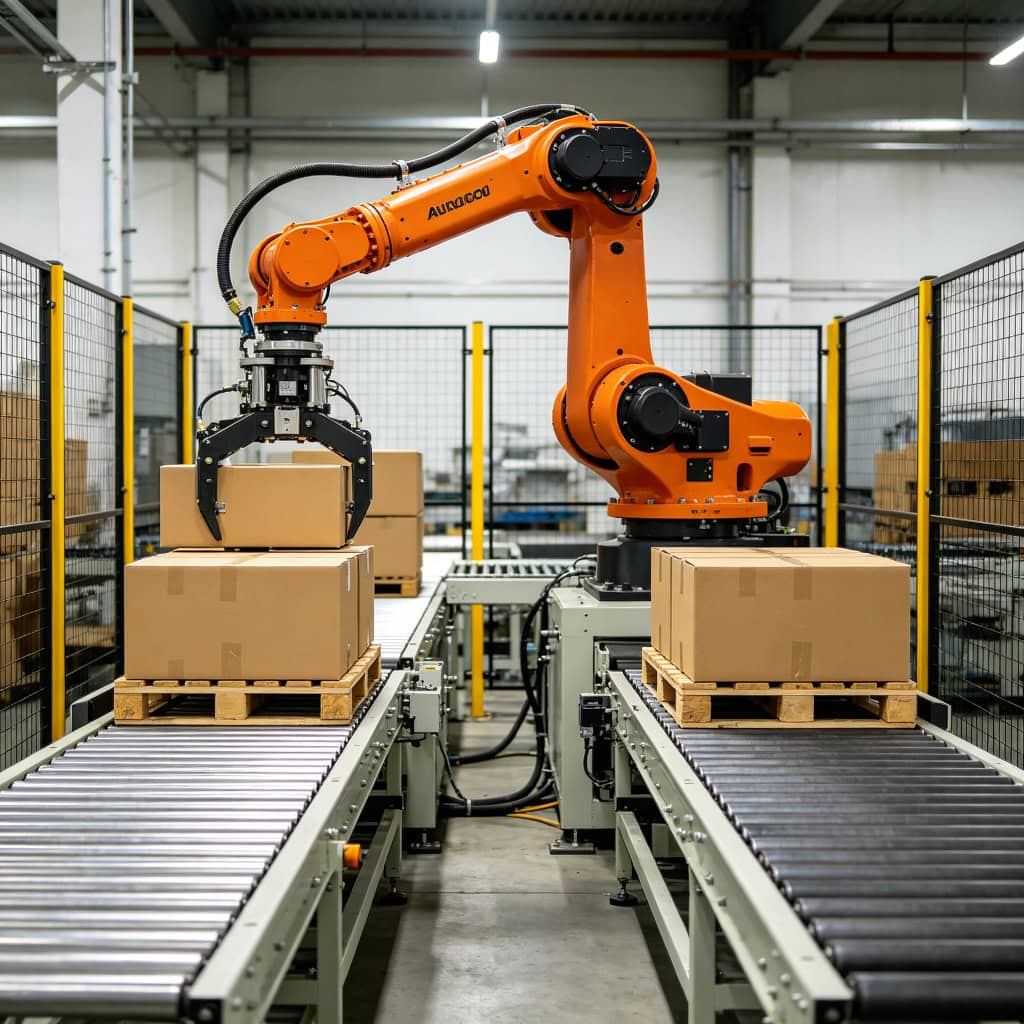
The SunAura heavy-duty four-axis robotic palletizer is engineered for the loads and environments that defeat standard robots: 25–50kg cement, mortar, fertilizer, flour and chemical bags, stacked to multi-layer pallets in dusty, abrasive, occasionally wet production halls. This is not a general-purpose arm pressed into heavy service — it is a purpose-built 4-axis palletizing robot with a reinforced wrist, over-sized bearings, and IP65 protection so dust and water spray cannot get into the drives.
Its 180kg payload and 2600mm reach let it pick a heavy bag (or two lighter bags together) and place it across a full standard pallet at up to 12 cycles per minute. Repeatability is ±0.8mm — looser than the lighter 120kg model, but more than enough for coarse bag patterns where bags are deliberately laid in overlapping rows. A heavy-duty mechanical gripper EOAT cradles the bag body and folds the corners under as needed to build a stable brick pattern. The arm is bolted to a reinforced pedestal foundation, and the cell includes interlocked safety fencing for continuous unattended operation.
Powered by 380V 3-phase, the cell is designed for multi-shift, high-duty-cycle operation in cement, fertilizer, chemical, building-material and mineral processing. Every unit undergoes a 48-hour continuous run test before shipment and ships CE certified. Send us your bag samples, pallet size and hourly output — our engineers will specify the gripper and test the bag pattern before you order.
Technical Specifications
| Model | SNA-RP180 Heavy-Duty Four-Axis Robotic Palletizer |
|---|---|
| Robot Type | 4-axis heavy-duty palletizing robot, reinforced wrist |
| Payload | 180 kg (product + EOAT combined) |
| Max Reach | 2600 mm |
| Cycle Rate | Up to 12 cycles per minute |
| Repeatability | ±0.8 mm |
| End-of-Arm Tool | Heavy-duty mechanical bag gripper (reinforced) |
| Protection Rating | IP65 (dust-tight, water-spray protected) |
| Voltage | 380V 3-phase, 50/60 Hz (factory-set to order) |
| Safety | Interlocked safety fencing + reinforced pedestal mounting |
| Control | PLC + touchscreen HMI, multi-recipe bag pattern storage |
| Certification | CE Certified, ISO 9001 factory |
Key Features & Benefits
- 180kg heavy-duty payload: Handles 25–50kg cement, fertilizer and chemical bags with ease, and can pick two lighter bags together for higher effective throughput.
- Reinforced wrist and over-sized bearings: The wrist and joint bearings are upsized for repeated heavy lifts and the side loads of gripping soft bags — longer service life in abrasive duty.
- IP65 dust-tight protection: Drives and arm are sealed against cement dust and water spray, so the robot keeps running in the dusty, washdown-prone environments that would disable a standard IP54 arm.
- Heavy-duty bag gripper EOAT: A reinforced mechanical gripper holds the bag body and can fold bag corners to form tight, stable brick patterns that do not collapse under their own weight.
- 2600mm reach for tall, wide loads: Reaches the far edges of a full standard pallet and builds tall multi-layer bag stacks without needing a track or second cell.
- High-duty-cycle construction: Designed for multi-shift, near-continuous operation in cement, fertilizer and mineral plants where the machine runs when the line runs.
- Recipe-driven bag patterns: Store bag dimensions and stacking patterns by product on the HMI. Operators select by name for quick changeover between bag types.
Application Industries
Cement & Concrete
25–50kg cement bags and dry-mix sacks — IP65 dust-tight arm and reinforced wrist handle the most abrasive bag duty in the industry.
Fertilizer & Agrochemical
Bags of NPK fertilizer, urea and granular agrochemicals — builds stable rows on export pallets for long-distance shipping.
Chemicals
Sacks of powder, granules and additives — heavy-duty gripper and dust-sealed body protect workers and the machine from spillage.
Building Materials
Bags of mortar, grout, gypsum and putty — handles dusty, heavy construction-material bags at high duty cycles.
Minerals & Ore
Bags of mineral powders, sand and additives — robust construction tolerates grit and fine dust around the work area.
Food & Flour
Heavy bags of flour, sugar and animal feed — gentle gripper handling avoids bursting seams on food-grade woven bags.
Load compatibility: Heavy woven and paper bags, sacks and rigid bulk containers up to 180kg per pick. For lighter carton-only lines, the 120kg model offers better cycle economy.
How the Heavy-Duty Bag Palletizer Works
Bag palletizing differs from carton stacking because soft bags deform and must be laid in an overlapping brick pattern to stay stable. The cycle runs as follows:
- Bags arrive on the infeed conveyor. Filled bags come off the bagging machine and are separated and stopped at the pick station, often flattened by a pre-conditioning conveyor.
- Heavy-duty gripper picks the bag. The reinforced mechanical jaws close around the bag body; corner folders (if fitted) tuck the bag ends for a tighter, more stable placement. A grip sensor confirms the hold.
- Arm carries the heavy bag to the pallet. The 180kg arm swings the bag across the work envelope, keeping it level so powder or granules do not shift inside the bag.
- Bag laid in the overlapping brick pattern. The arm places each bag to overlap the row below, building a self-supporting wall. The HMI advances the pattern and counts rows and layers.
- Layer complete — pallet grows. The arm descends to the new layer height and continues. Slip sheets may be inserted between layers on request. When the pallet reaches its programmed height, the cell signals for a forklift to remove the loaded pallet.
Is This the Right Palletizer for You?
This 180kg heavy-duty robot is the right fit if your operation matches all four of the following. If you fall outside any of them, our team can recommend a different SunAura model:
- Heavy bags or bulk loads up to 180kg: This arm is sized for 25–50kg (and up to 180kg) heavy bags, drums and bulk containers. If you palletize light cartons under 50kg, the 120kg or dual-station robot gives you faster cycles at lower cost.
- Dusty, abrasive or washdown-prone environment: IP65 protection and a sealed arm are essential in cement, fertilizer and mineral plants. For a clean, dry room running cartons, IP54 is overkill — the 120kg model suffices.
- Throughput around 10–12 bag cycles/min: The heavy arm is durable but not as fast as lighter robots because of the mass it accelerates. For the absolute highest bag throughput in a steady product, a dedicated automatic bag palletizer or gantry system may be faster.
- Multi-shift, near-continuous duty: The reinforced construction is built for when the machine runs most of the week. If you run light, intermittent shifts, a smaller robot is more economical to buy and run.
Troubleshooting Guide — Common Issues & Solutions
Heavy-duty bag palletizers run in some of the toughest factory conditions, so dust, wear and bag deformation are the recurring themes. Below are the most common problems we diagnose remotely. Always lock out and tag out energy before entering the fenced cell.
| Problem | Possible Causes | Solutions |
|---|---|---|
| Bag slips or tears in the gripper | Gripper pressure too high/low; jaw pads worn; bag damp or over-filled; corner folders mis-timed. |
|
| Stack leans or collapses mid-build | Brick pattern offset off; layer height wrong; bags not flattened before pick; no slip sheet on tall stacks. |
|
| Dust ingress / drive over-temp alarm | Arm seals compromised; cooling fans blocked with dust; motor overloaded; IP65 filter/panel damaged. |
|
| Reduced cycle speed / servo faults | Joint reducers worn from heavy duty; belt/chain tension off; encoder drift; over-temp drive. |
|
| Pallet not detected / wrong height | Height sensor caked in dust; pallet warped; empty pallet off-center; Z-axis offset drifted. |
|
| Infeed conveyor jams with bags | Bags overlapping or double-fed; pre-conditioner jammed; motor overload; side guides mis-set. |
|
If the issue persists after trying these steps, email photos and a short 10-second video to [email protected] — our engineers usually diagnose the root cause within one business day.
Frequently Asked Questions
How is the 180kg model different from your standard 120kg palletizer?
The 180kg model is built heavier and more sealed: 180kg payload (vs 120kg), 2600mm reach (vs 2400mm), a reinforced wrist and over-sized bearings, and IP65 dust-tight protection (vs IP54). Repeatability is ±0.8mm rather than ±0.5mm, because coarse bag patterns do not need carton-level precision. It is purpose-built for the heaviest, dustiest bag duty; the 120kg model is the versatile general-purpose arm.
What bag weights and sizes can it handle?
The 180kg rating covers 25–50kg cement, fertilizer and chemical bags as standard, and up to roughly 180kg total per pick including the gripper. It can also pick two lighter bags at once for higher throughput. Send us your bag dimensions and weight and we confirm the gripper design and pattern.
Does the dusty cement environment damage the robot?
This is exactly why the arm is rated IP65 — dust-tight and water-spray protected. Joints, cable glands and the cabinet are sealed so cement dust cannot enter the drives. We still recommend routine blow-out of cooling fans and cabinet filters, and we provide a maintenance schedule. The reinforced wrist and bearings are specified for abrasive, high-duty operation.
How many bags per hour can it palletize?
The arm completes up to 12 cycles per minute. Actual bag throughput depends on bag weight, reach distance and whether corner-folding is used — typically around 600–720 bags per hour. For the absolute highest bag volumes on a steady product, we can pair it with a dual-station arrangement or recommend a dedicated automatic bag palletizer.
What is the warranty and lead time?
Every unit carries a 12-month warranty covering parts and labor, plus lifetime technical support by email and WhatsApp. Heavy-duty cells ship in 35–50 days; custom gripper and foundation configurations take 50–70 days. Each machine runs a 48-hour continuous test and ships with CE documentation.
Why Buy From SunAura Machinery
48,000㎡ Own Factory
In-house manufacturing in Qingdao, China — no middlemen, no trader markup.
CE Certified
All machines meet European safety standards with full documentation.
ISO 9001:2015
Quality management system certified across the entire production process.
SGS Audited Factory
Third-party audited manufacturing facility with 20+ national patents.
12-Month Warranty
Full warranty covering parts and labor from the date of shipment.
Lifetime Support
Technical guidance via email, WhatsApp, and remote video for the machine’s life.
Spare Parts in 48h
Genuine parts shipped worldwide via DHL/FedEx within 48 hours.
100+ Countries Served
Trusted by packaging lines across food, pharma, cosmetics, and chemicals.
Get a Factory-Direct Quote in 24 Hours
Tell us your bag size and weight, pallet dimensions, and hourly output — our engineers reply with a model recommendation, gripper selection, FOB price, and lead time within one business day. Every machine is built in our 48,000㎡ Qingdao factory, CE & ISO 9001 certified.
Email [email protected]Related Palletizers
Browse the full range on the palletizers landing page. Also explore our induction sealers and filling machines to build a complete packaging line.